
Product Description
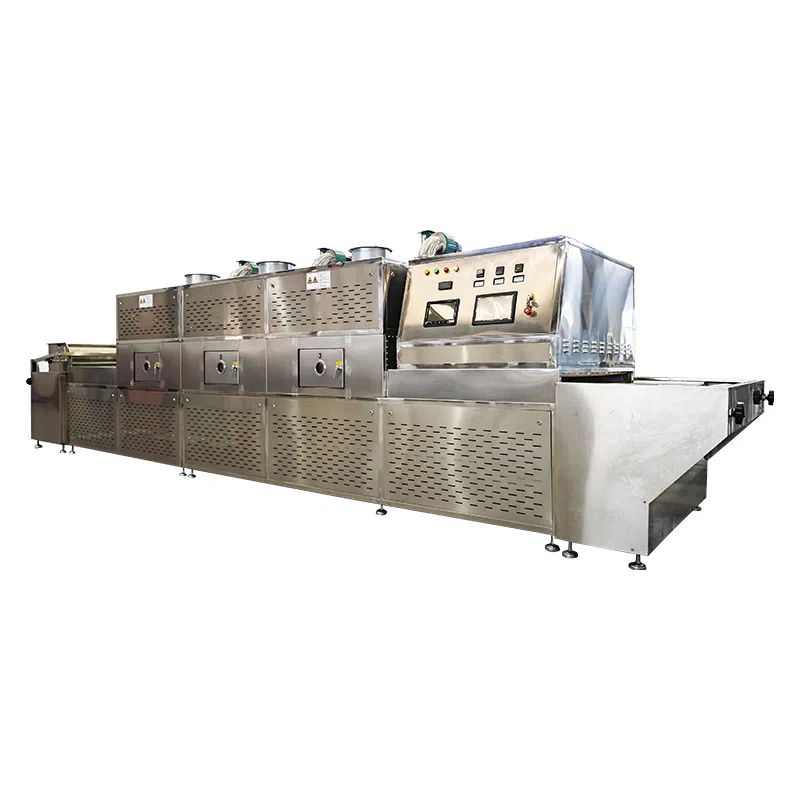
The box‑lunch microwave heating equipment adopts high‑frequency 2450 MHz microwave energy, which directly acts on polar water molecules inside box‑lunch meals, group‑catering boxed food, high‑speed‑rail fast‑food, canteen boxed meals, central‑kitchen portioned dishes and sealed ready‑to‑eat lunch boxes. Water molecules vibrate, rub and collide at an ultra‑high frequency of 2.45 billion times per second, converting electromagnetic energy into thermal energy to achieve fast volumetric inside‑out reheating and pasteurization for box‑lunch products.
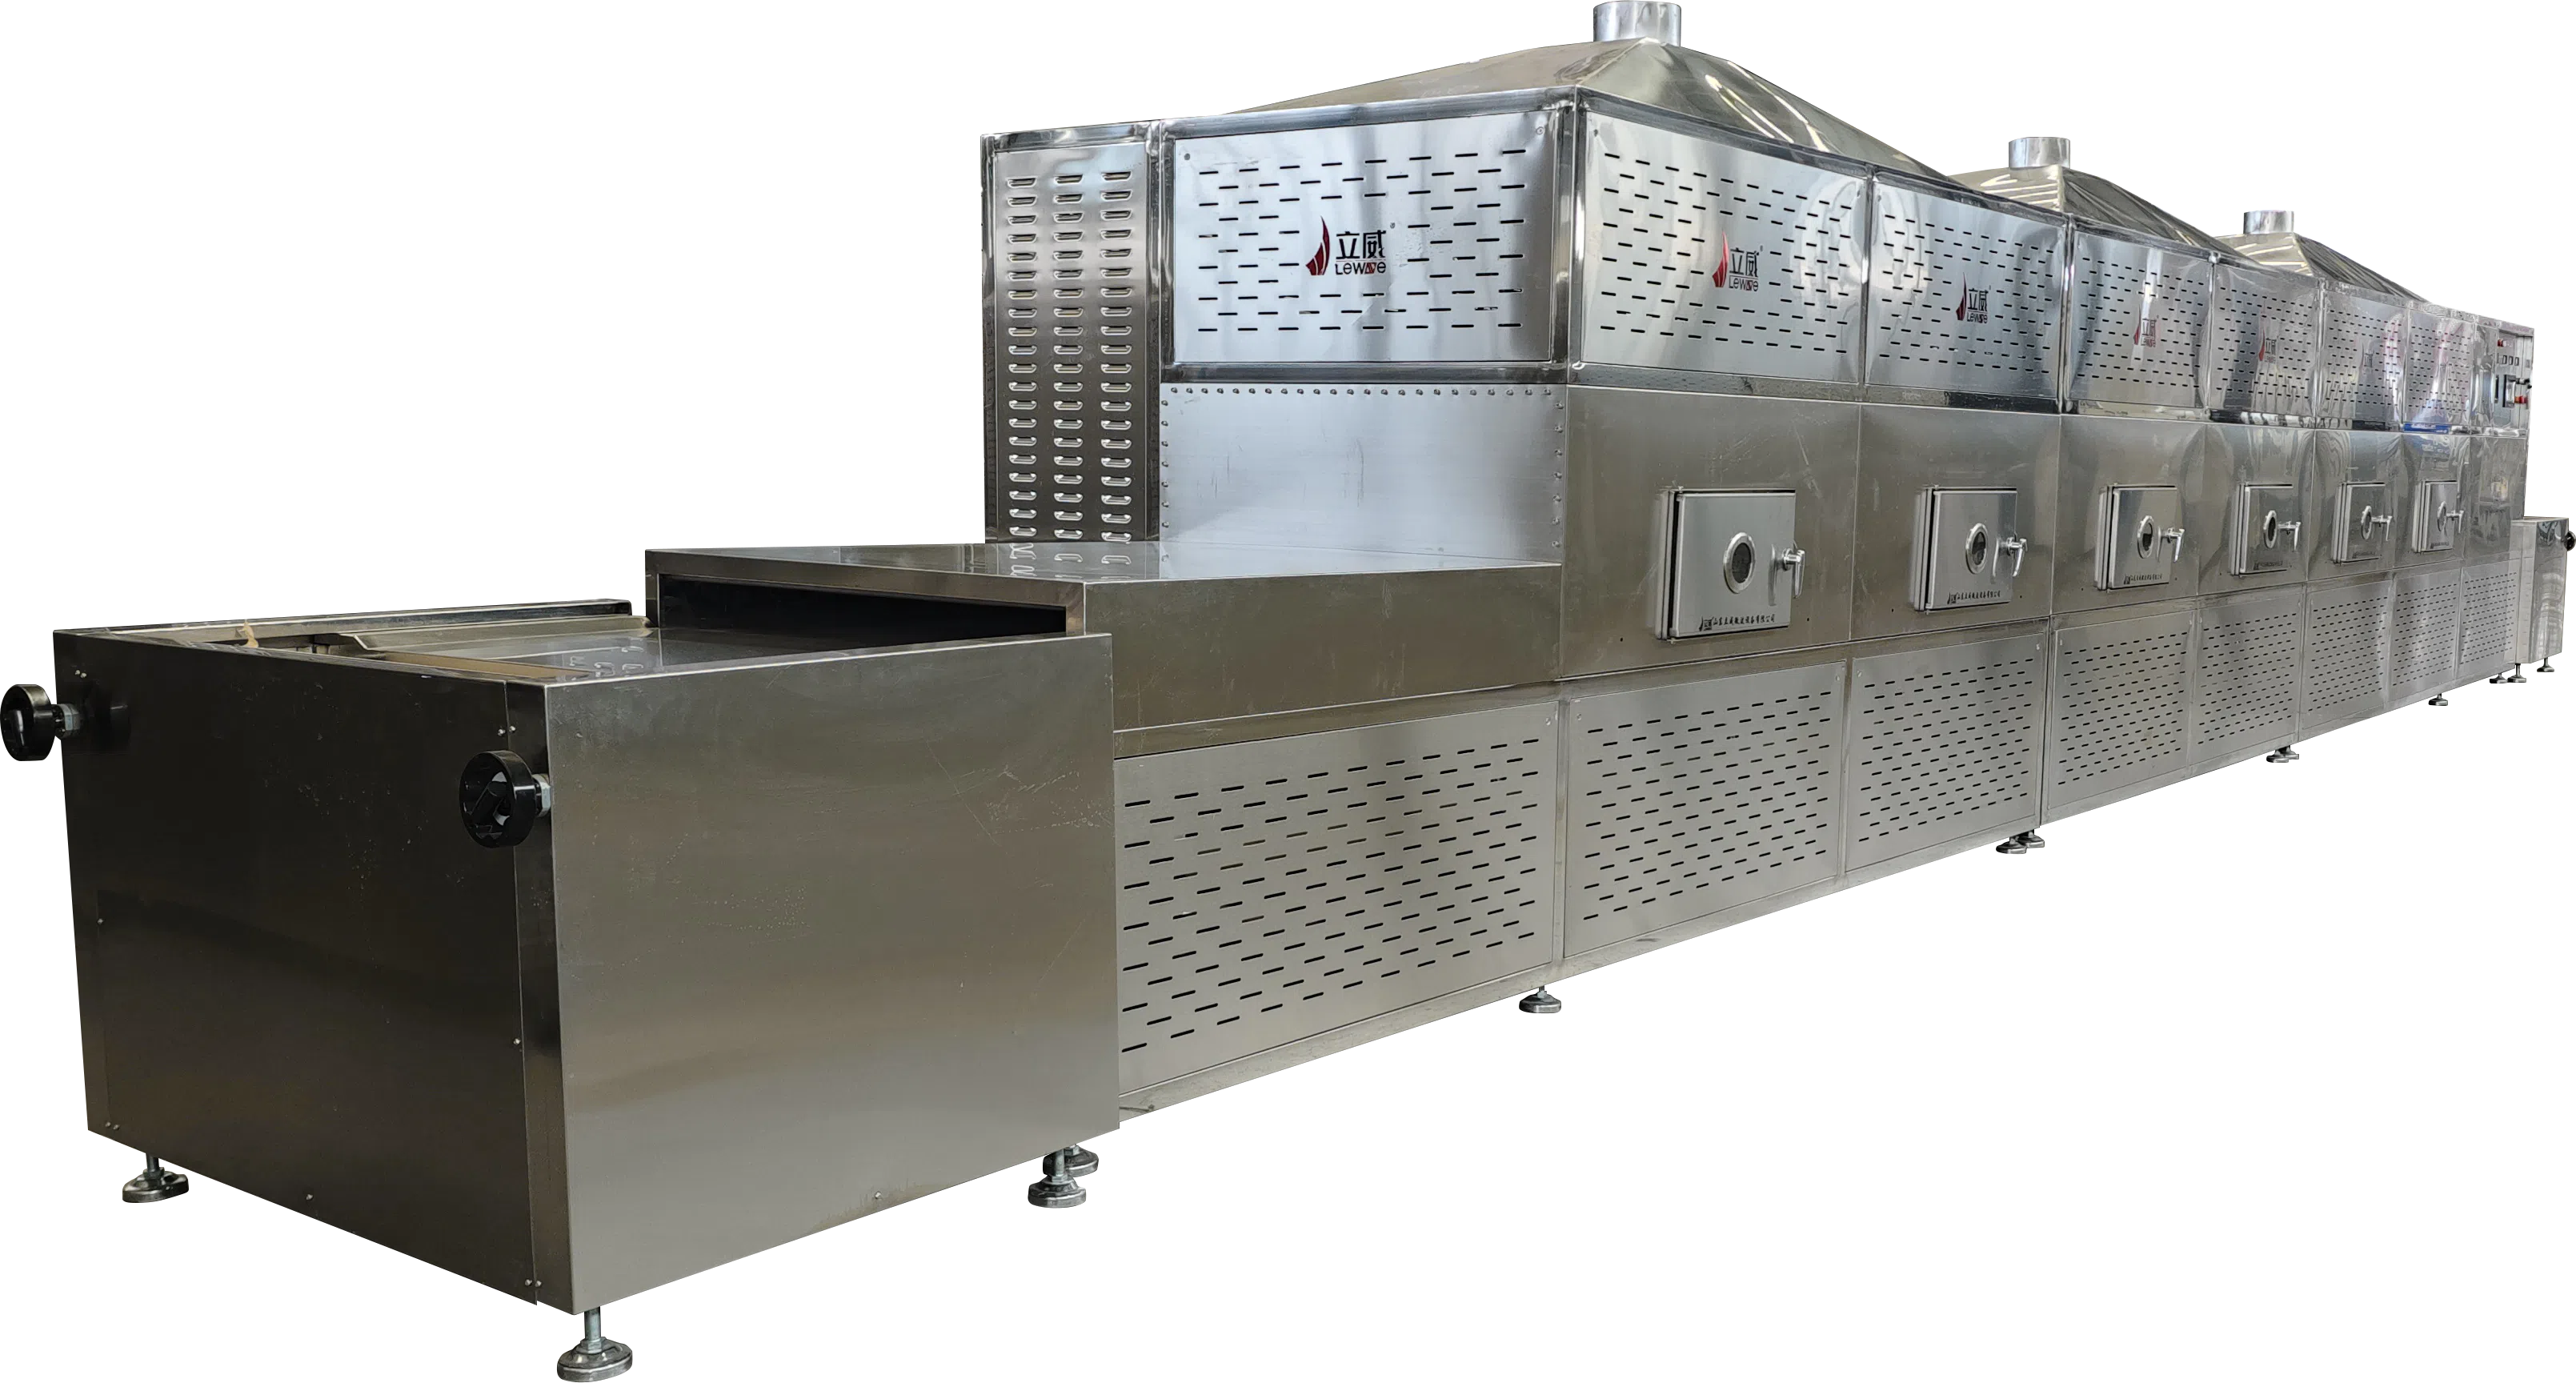
Different from traditional steam ovens and hot‑air tunnels relying on surface heat conduction, microwave delivers strong penetrating volumetric heating. It effectively solves typical industry pain‑points: over‑heated surface while food core remains cold, dried rice, mushy vegetables, uneven temperature distribution, sauce loss and inconsistent batch quality of box‑lunch meals.
During operation, sealed lunch boxes are orderly placed on food‑grade wear‑resistant conveyor belt and continuously transported into multi‑cascaded microwave tunnel cavities with adjustable speed. Microwaves penetrate the lunch‑box container and heat rice, meat and vegetables simultaneously from inside to outside, rapidly raising food core temperature and inhibiting harmful bacteria. The matched exhaust‑dehumidification system timely discharges water vapor, completing continuous integrated reheating and pasteurization in one production pass.
Homogeneous microwave thermal field avoids local over‑cooking. It retains moisture, original flavor and nutritional components of box‑lunch food, keeps rice soft and vegetables well‑textured. It improves food safety for group catering, cold‑chain distribution and large‑volume meal supply.
Main Advantages
Volumetric Inside‑out Heating, Uniform Reheating for Mass Box‑Lunch Production Adopts molecular volumetric heating instead of surface heat transfer. Each lunch box is heated from inside to outside, eliminating cold core, scorched edges, hard rice and uneven temperature. Processed box‑lunches feature stable taste and consistent temperature, greatly raising finished‑product qualification rate for large‑scale group‑meal production.
Rapid Short‑time Heating, Preserve Original Taste & Nutrients No pre‑heating required for startup. Short‑time rapid reheating reduces nutrition loss caused by long‑time thermal treatment. Rice stays soft, vegetables do not get over‑cooked, sauce loss is minimized. Especially suitable for large‑batch chilled box‑lunches, central‑kitchen group meals and high‑volume catering projects with strict taste requirements.
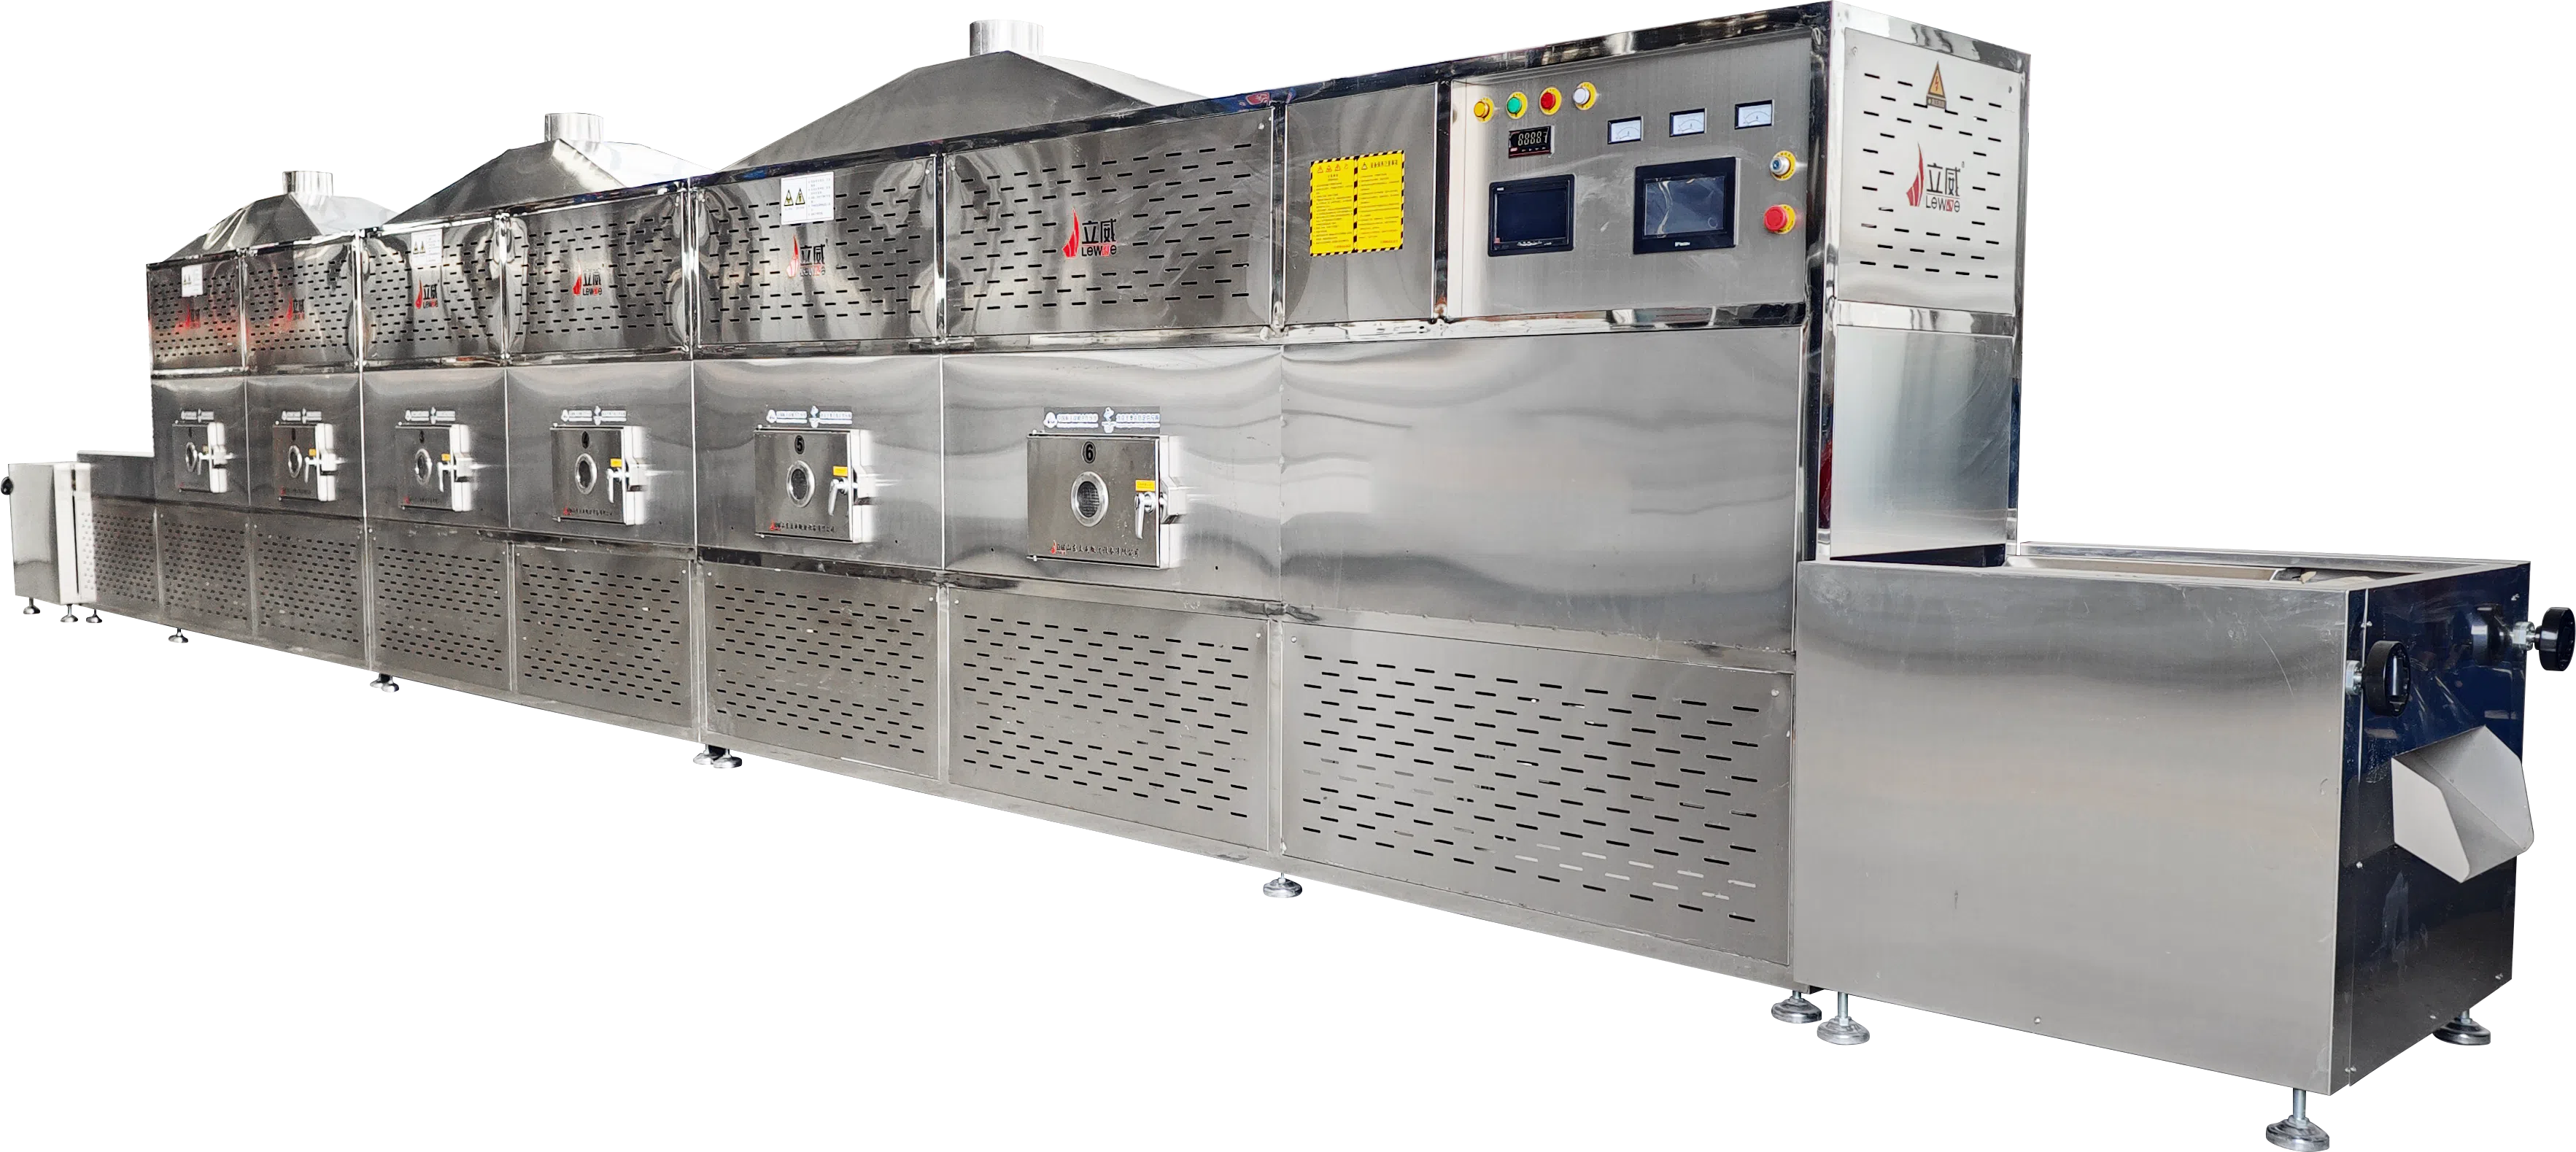
PLC Intelligent Adjustable Process, Adaptable for Various Lunch‑Box Specifications Equipped with PLC touch‑screen control system; microwave power, conveyor speed, cavity temperature and exhaust air volume support stepless adjustment. It fits different‑size sealed lunch boxes, chilled or pre‑cooled group‑meal boxes. Multiple processing recipes can be stored for quick switching. Modular integrated structure supports long‑time continuous running with convenient parameter debugging and daily maintenanceAlibaba.co....
Continuous Automatic Production, Synchronous Pasteurization & High Throughput Multi‑stage microwave suppressors at inlet and outlet ensure microwave leakage complies with international safety standards. Fully‑automatic tunnel assembly‑line supports non‑stop continuous operation with large hourly throughput. It can be docked with upstream box‑packing and downstream conveying lines. Microwave realizes synchronous pasteurization to suppress mould and pathogenic bacteria, improving food safety for canteens, high‑speed‑rail catering and export‑oriented box‑meal products.
Equipment Composition
The box‑lunch microwave heating equipment is fully‑automatic tunnel‑type conveyor assembly‑line constructed with SUS304 food‑grade stainless‑steel modular design, complying with commercial catering food‑processing hygiene standards. The complete set includes feeding station, lunch‑box positioning section, multi‑cavity microwave heating tunnel, exhaust dehumidification system, online infrared temperature detection, microwave leakage suppression device, PLC intelligent control cabinet and automatic discharging unit. It is specially designed for large‑scale standardized continuous reheating and pasteurization of various sealed box‑lunch meals.
Application Fields
Custom‑developed for central kitchens, campus canteens, group‑catering enterprises, high‑speed‑rail catering service providers, large‑event meal suppliers and fast‑food factories. Widely used for continuous microwave reheating and pasteurization of box‑lunch products. Treated lunch boxes achieve uniform core temperature and high food‑safety level.


