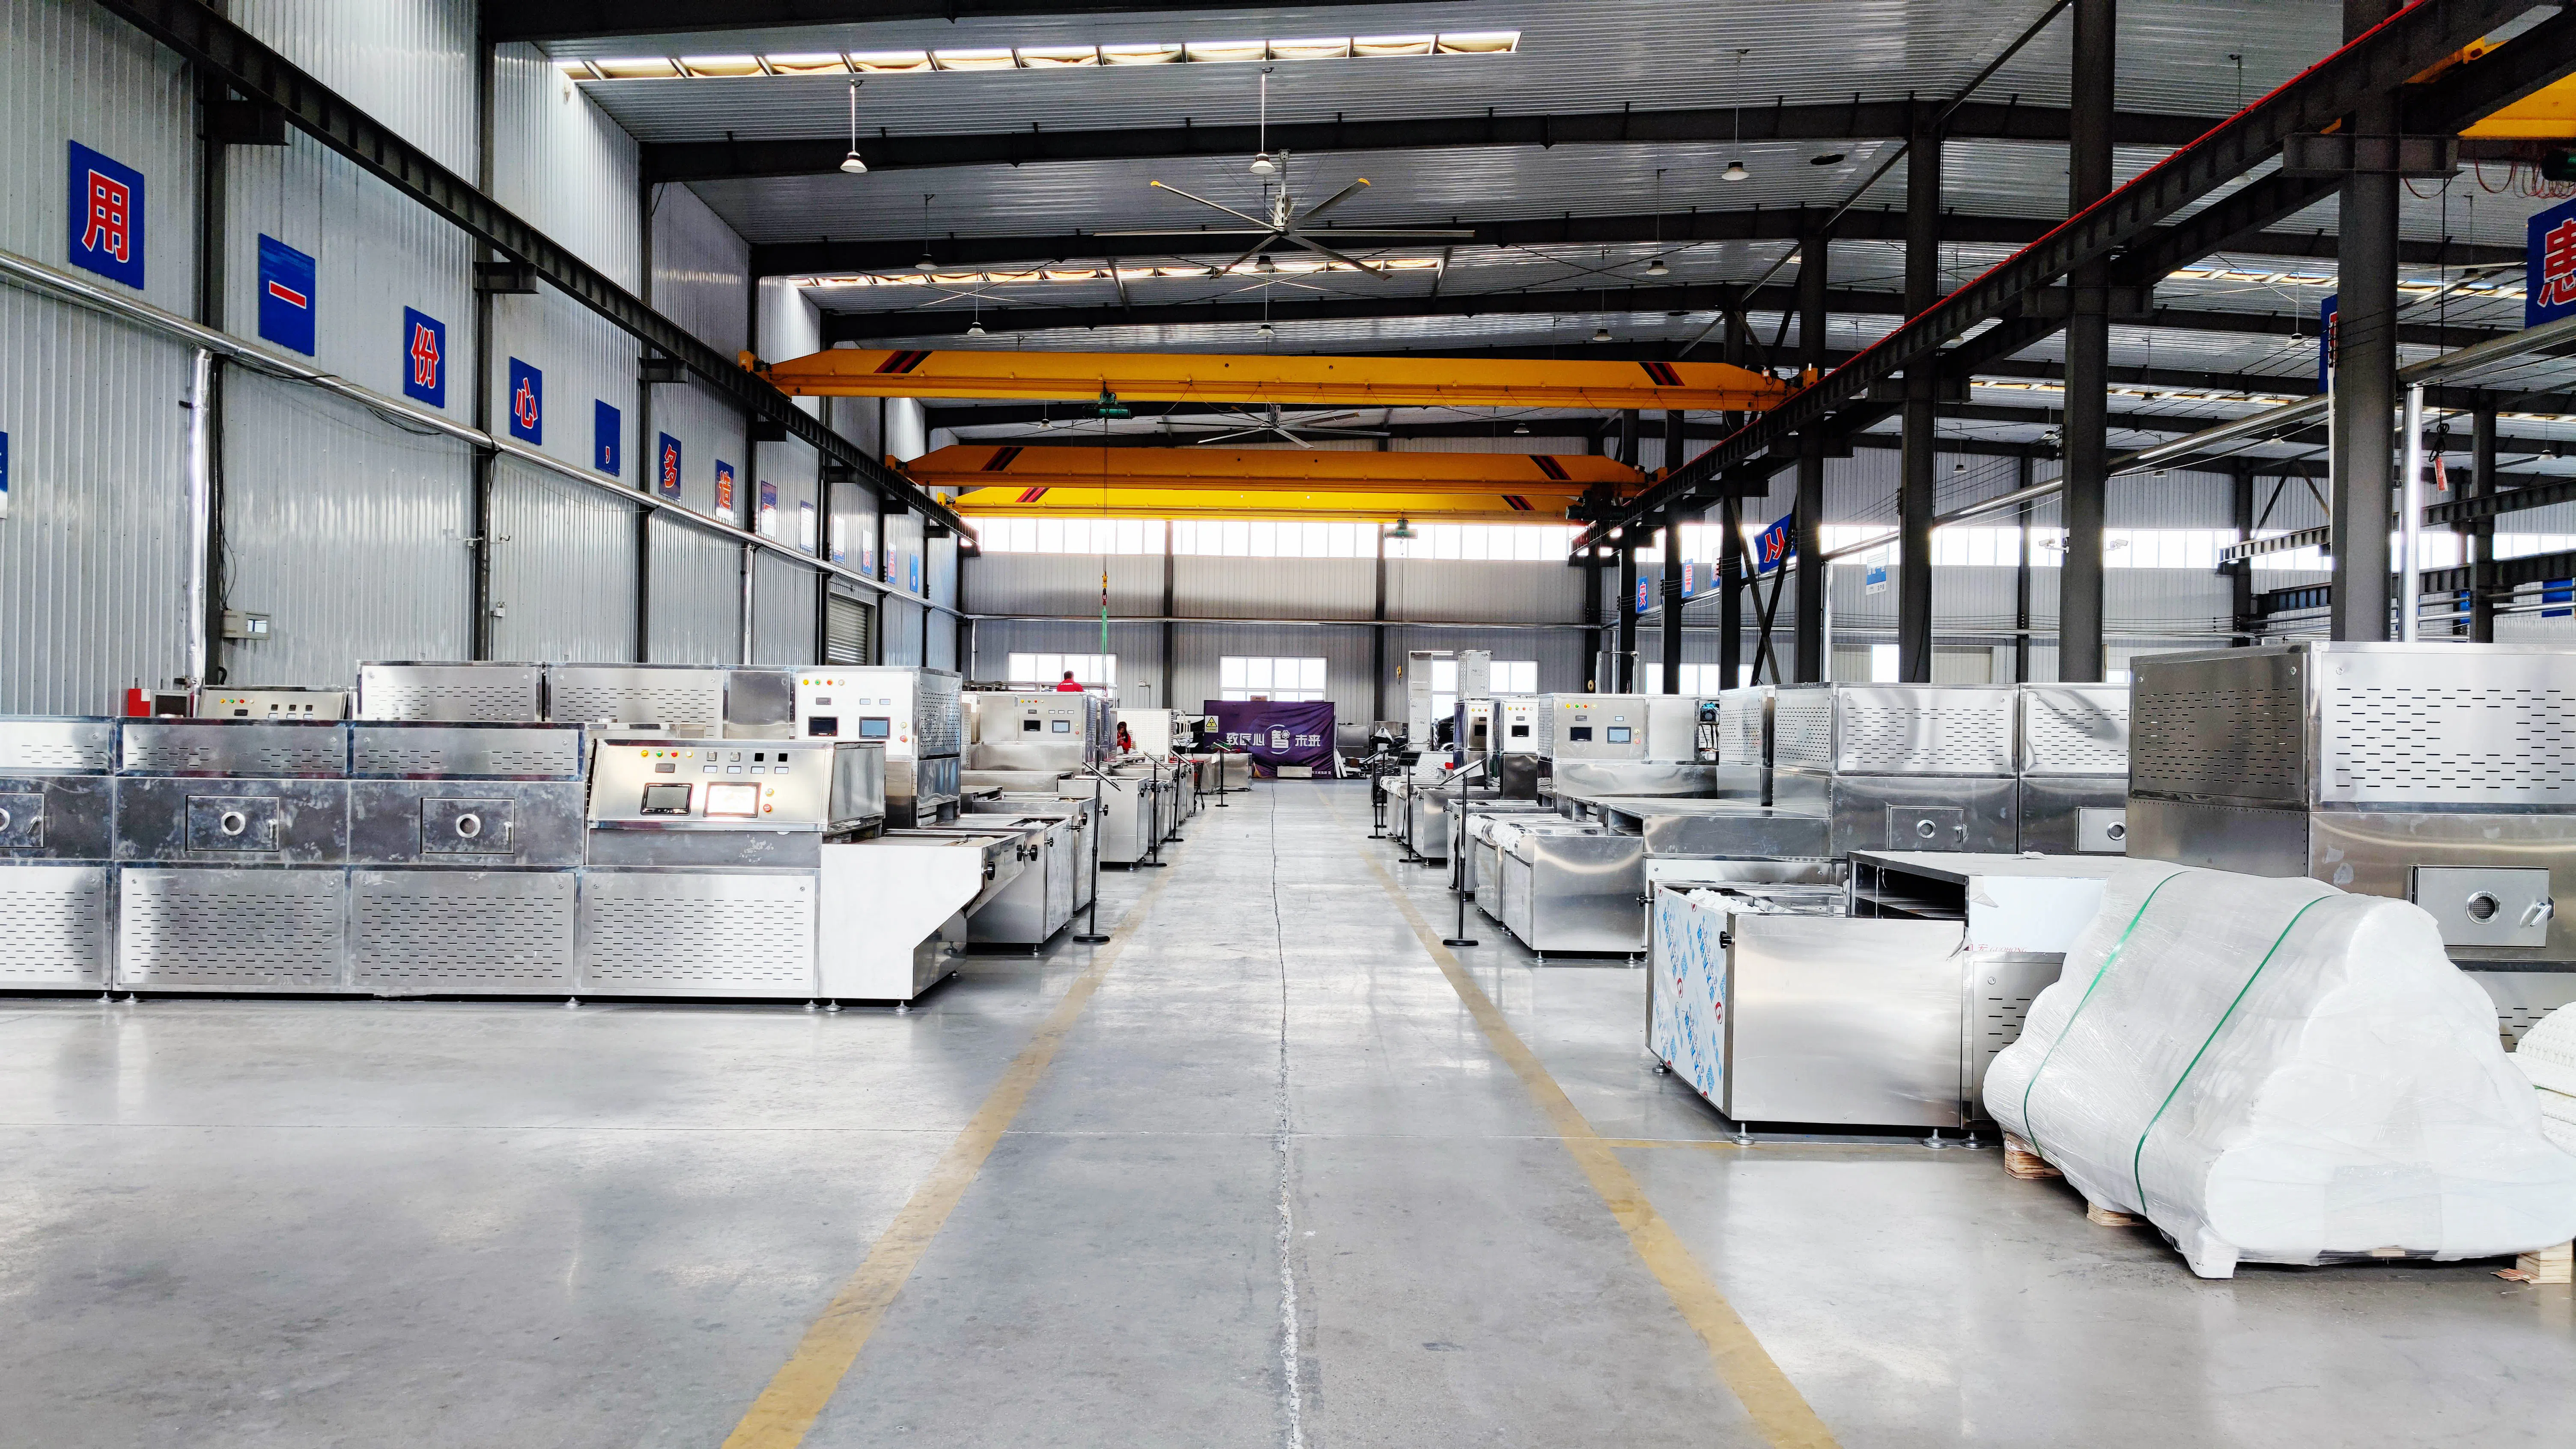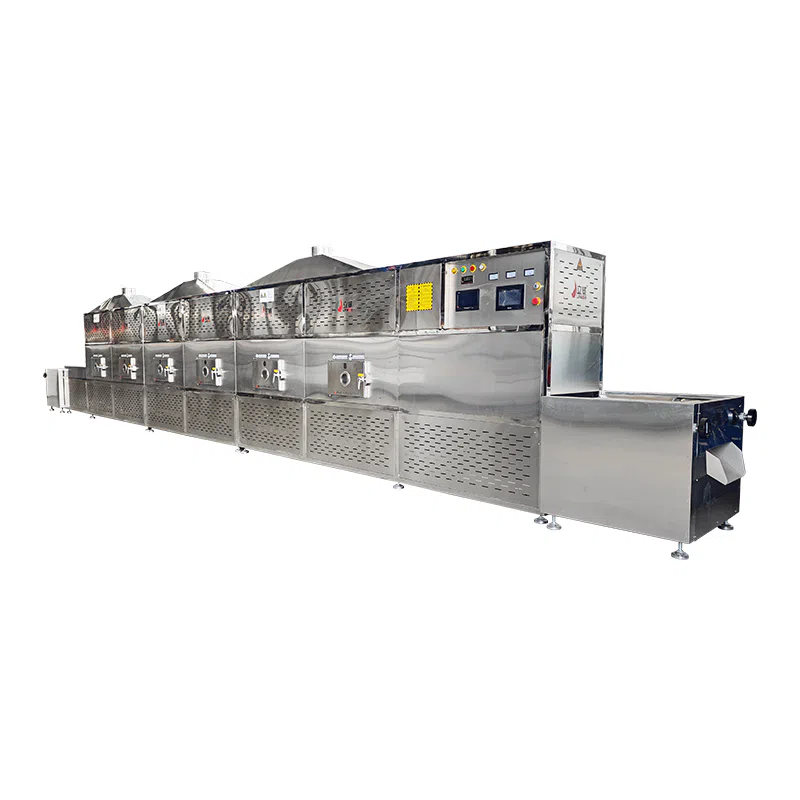
Product Description
This continuous tunnel microwave sanitization system is a specialized industrial microwave sterilization equipment built for post-fermentation food processing. Fermented food carries abundant fermented aroma metabolites and bioactive ingredients, yet conventional retort sterilization and traditional thermal sterilization will destroy fermented flavour profiles and functional nutrients. This industrial microwave sanitizing equipment adopts dielectric microwave heating technology to realize targeted microbial deactivation, delivering low-impact continuous sanitization while retaining the exclusive sensory attributes of fermented food products.
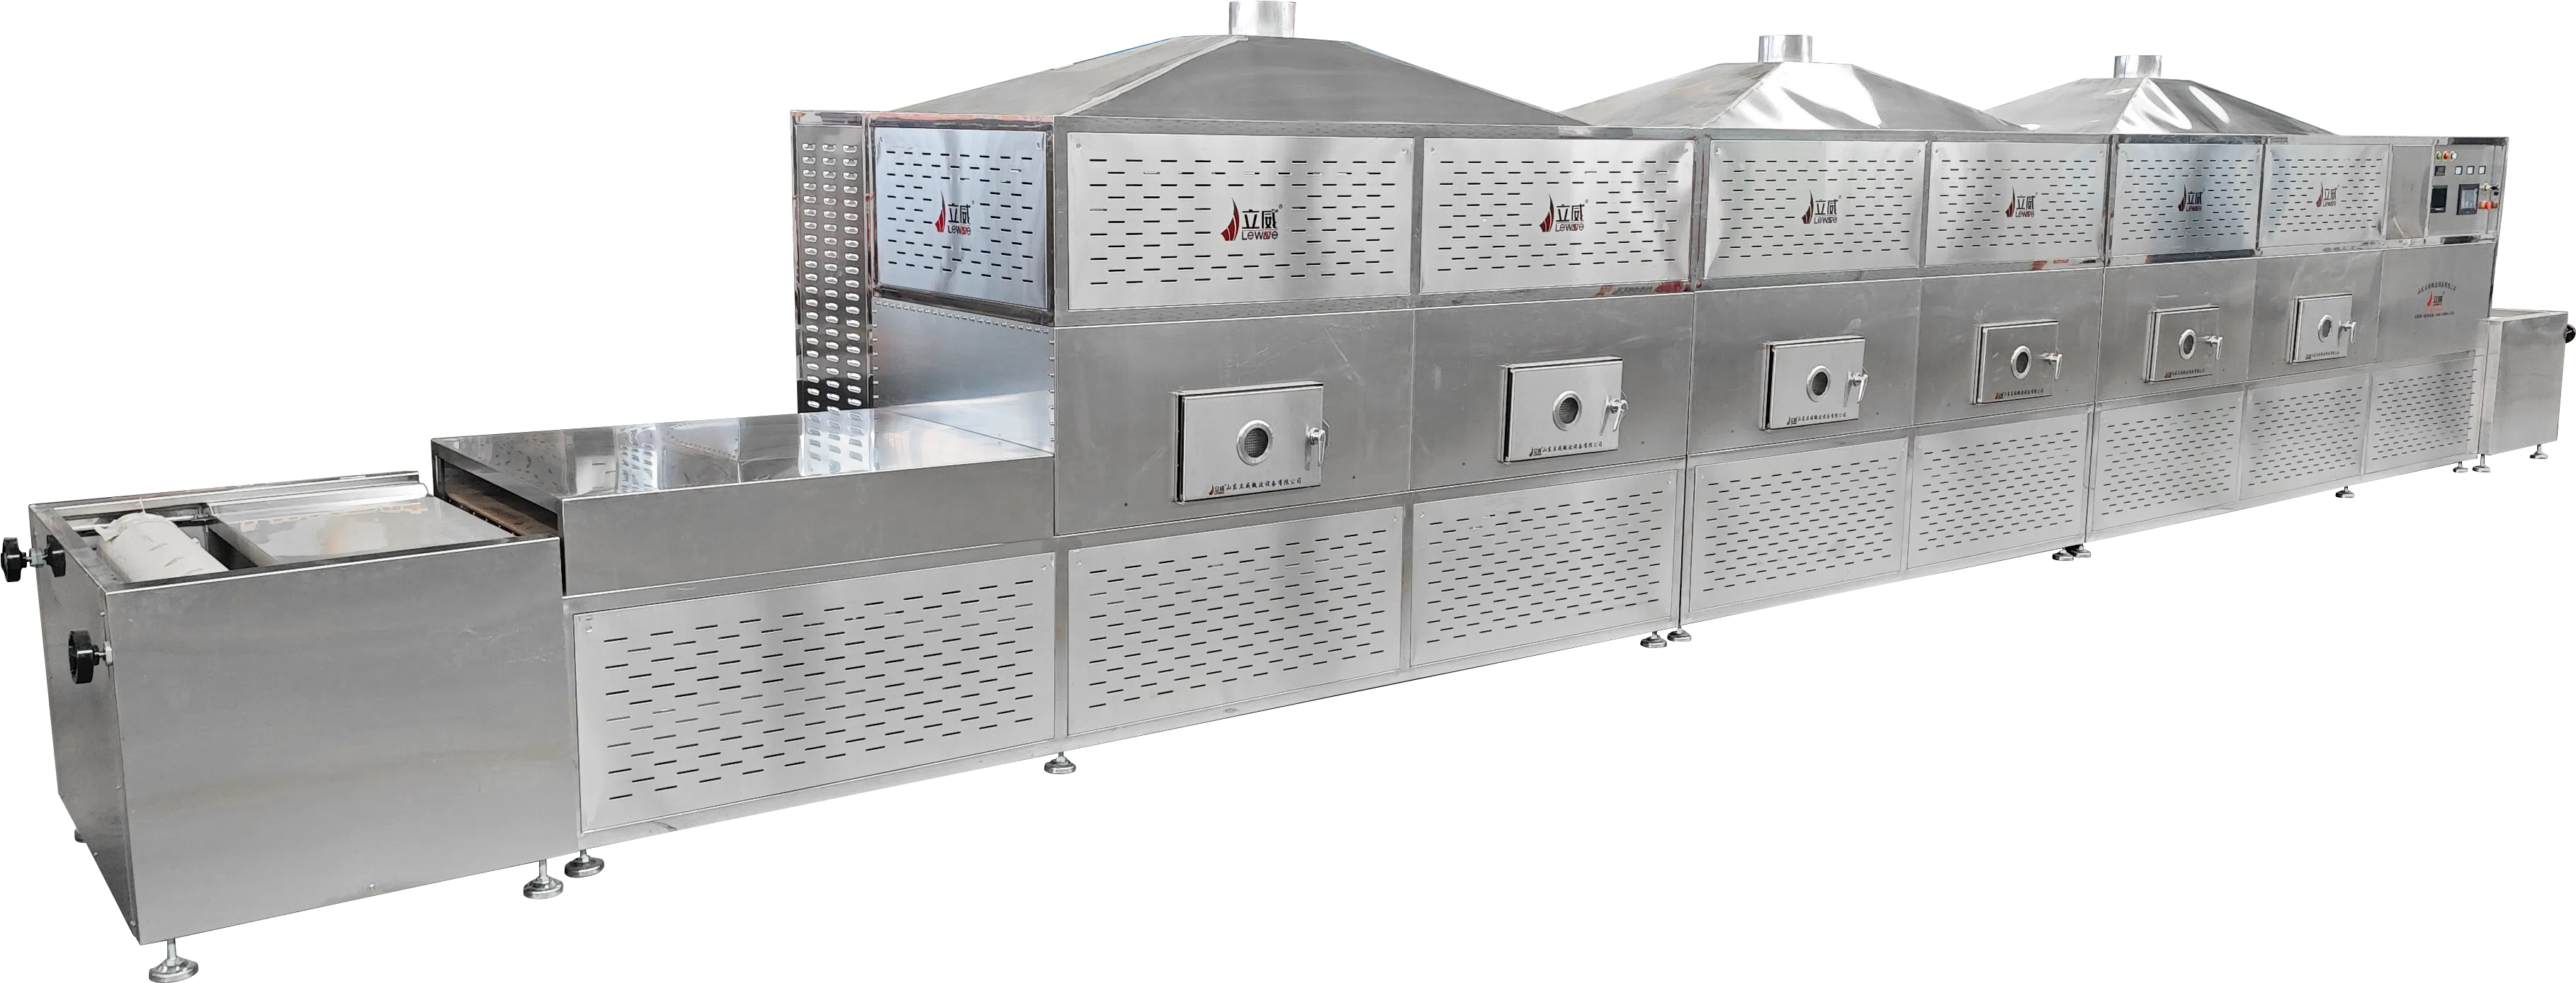
Microwave energy penetrates deep into fermented food substrates and drives vibration of polar water molecules to produce uniform internal dielectric heat within the food bed. Both unpackaged fermented bulk materials and pre-packaged fermented food move stably on food-grade conveyor belts into multi-cavity microwave sterilization tunnels. Precision closed-loop thermal control suppresses pathogenic bacteria, mould and spoilage yeast efficiently. The matched vapour exhaust dehumidification system discharges water vapour generated during microwave sanitization, supporting inline continuous microwave sterilization without severe thermal shock to fermented food matrices.
Core Strengths
Internal dielectric volumetric heating realizes homogeneous microbial killing across fermented food layers. It avoids the long-duration high heat exposure of retort sterilization, preserving fermented flavour, texture structure and heat-sensitive nutritional substances of fermented food.
Low-stress microwave sanitization parameters reduce food matrix collapse and volatile flavour loss, locking in the unique sensory features of fermented food and upgrading the commercial value of fermented finished products.
Intelligent PLC control system supports independent adjustment of microwave power and conveyor running speed, compatible with multiple fermented food varieties and different material paving thickness. All material contact components use food-grade materials to meet strict hygiene specifications of fermented food production lines.
Multi-layer shielding microwave cabins pass international microwave safety standards. Automatic tunnel continuous production improves throughput of bulk microwave sanitization, and fermented food after microwave treatment gains longer shelf life for domestic sales and export circulation.
Equipment Composition
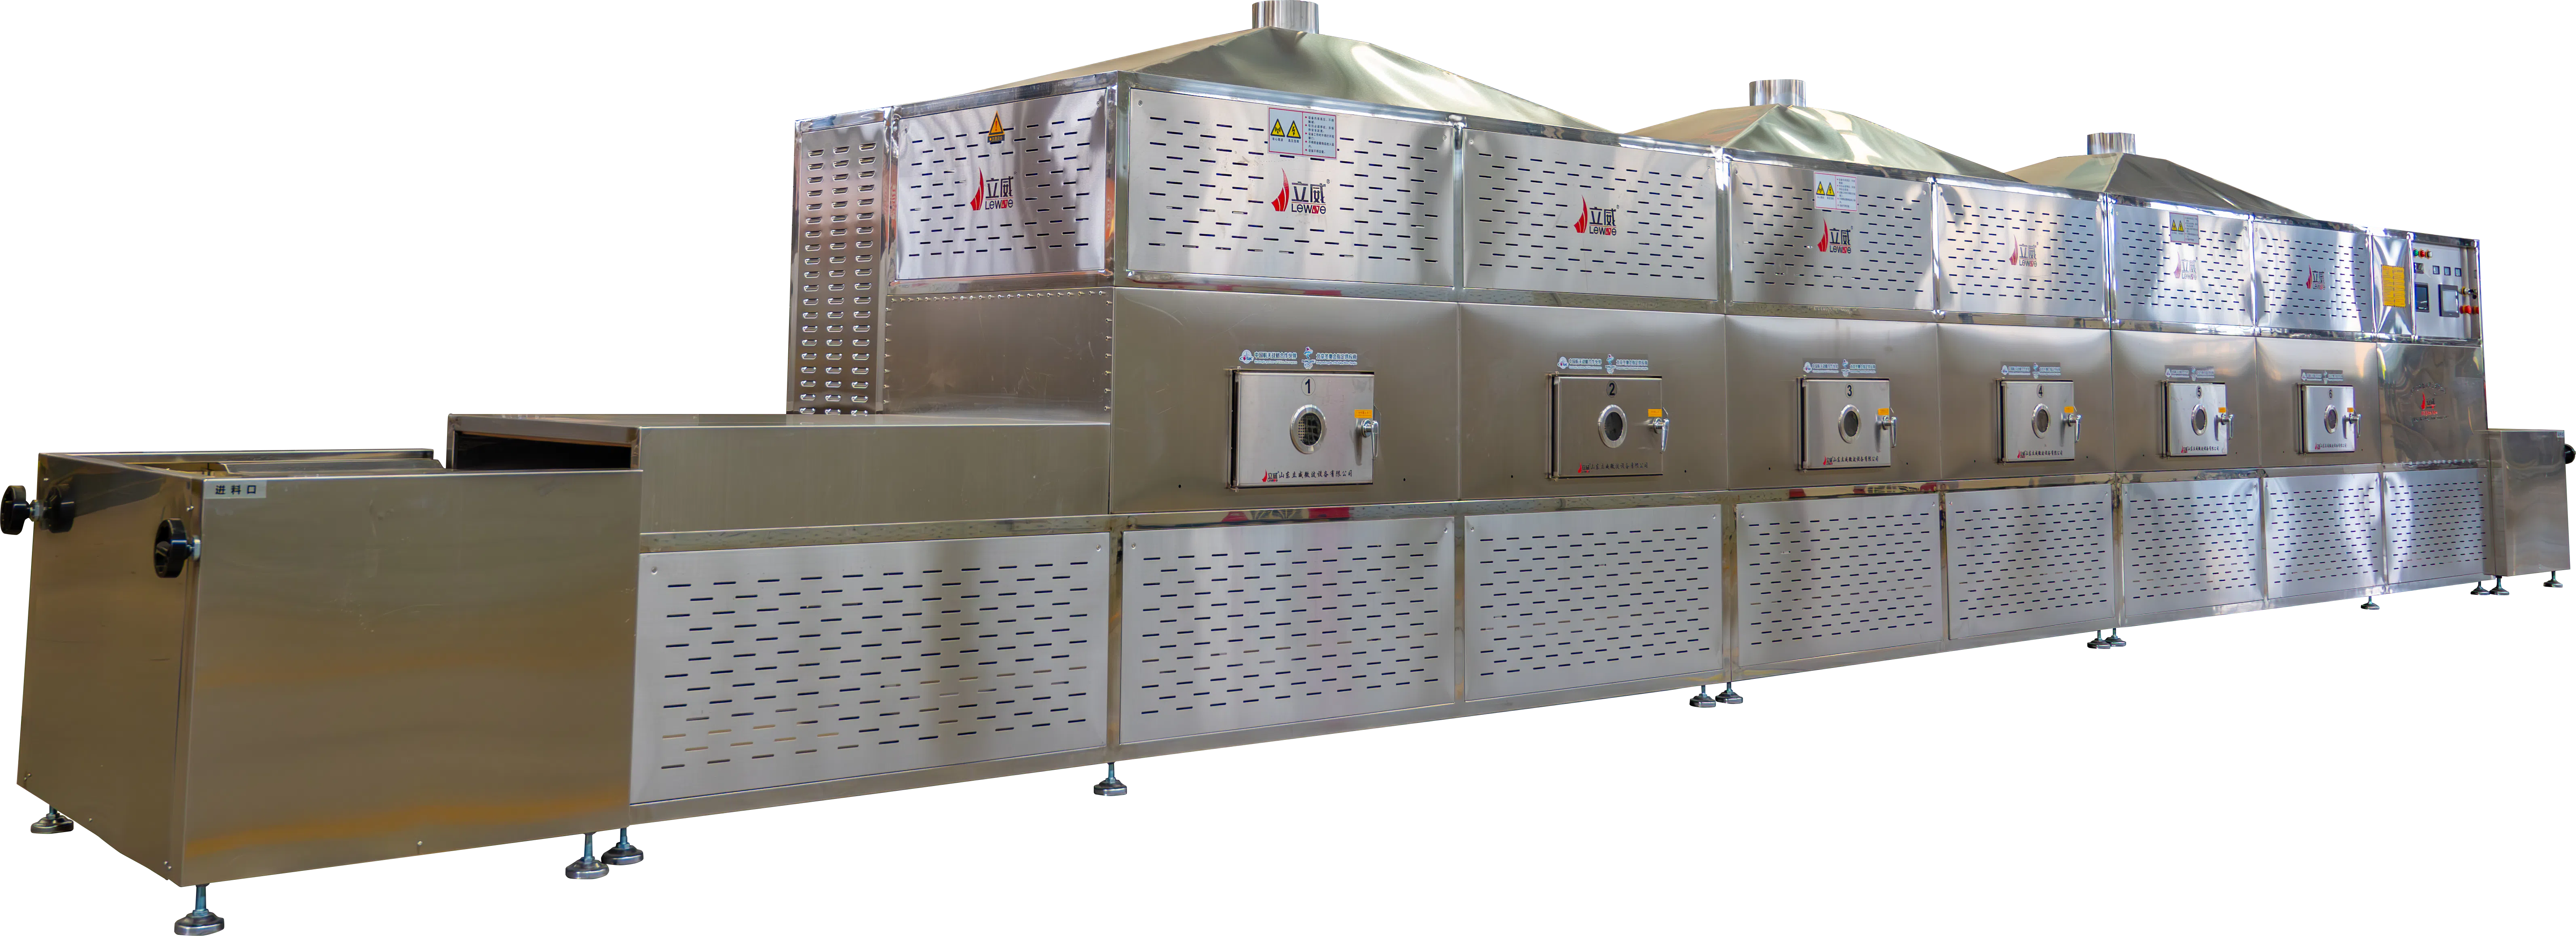
Component | Function |
|---|---|
Microwave Generator | Supplies microwave energy |
Processing Chamber | Provides the treatment environment |
Conveyor System | Moves fermented food products |
Feeding Unit | Controls product input |
Exhaust System | Removes heat and moisture |
Temperature Sensors | Monitor processing conditions |
PLC Control Cabinet | Manages machine operation |
Safety System | Provides equipment protection |
Application Fields
Fermented Soy Foods — Suitable for selected fermented soybean products.
Fermented Grain Foods — Applicable to compatible fermented grain products.
Fermented Bean Products — Used for controlled thermal treatment of selected bean-based fermented foods.
Prepared Fermented Foods — Suitable for downstream processing of compatible fermented food products.