Product Description
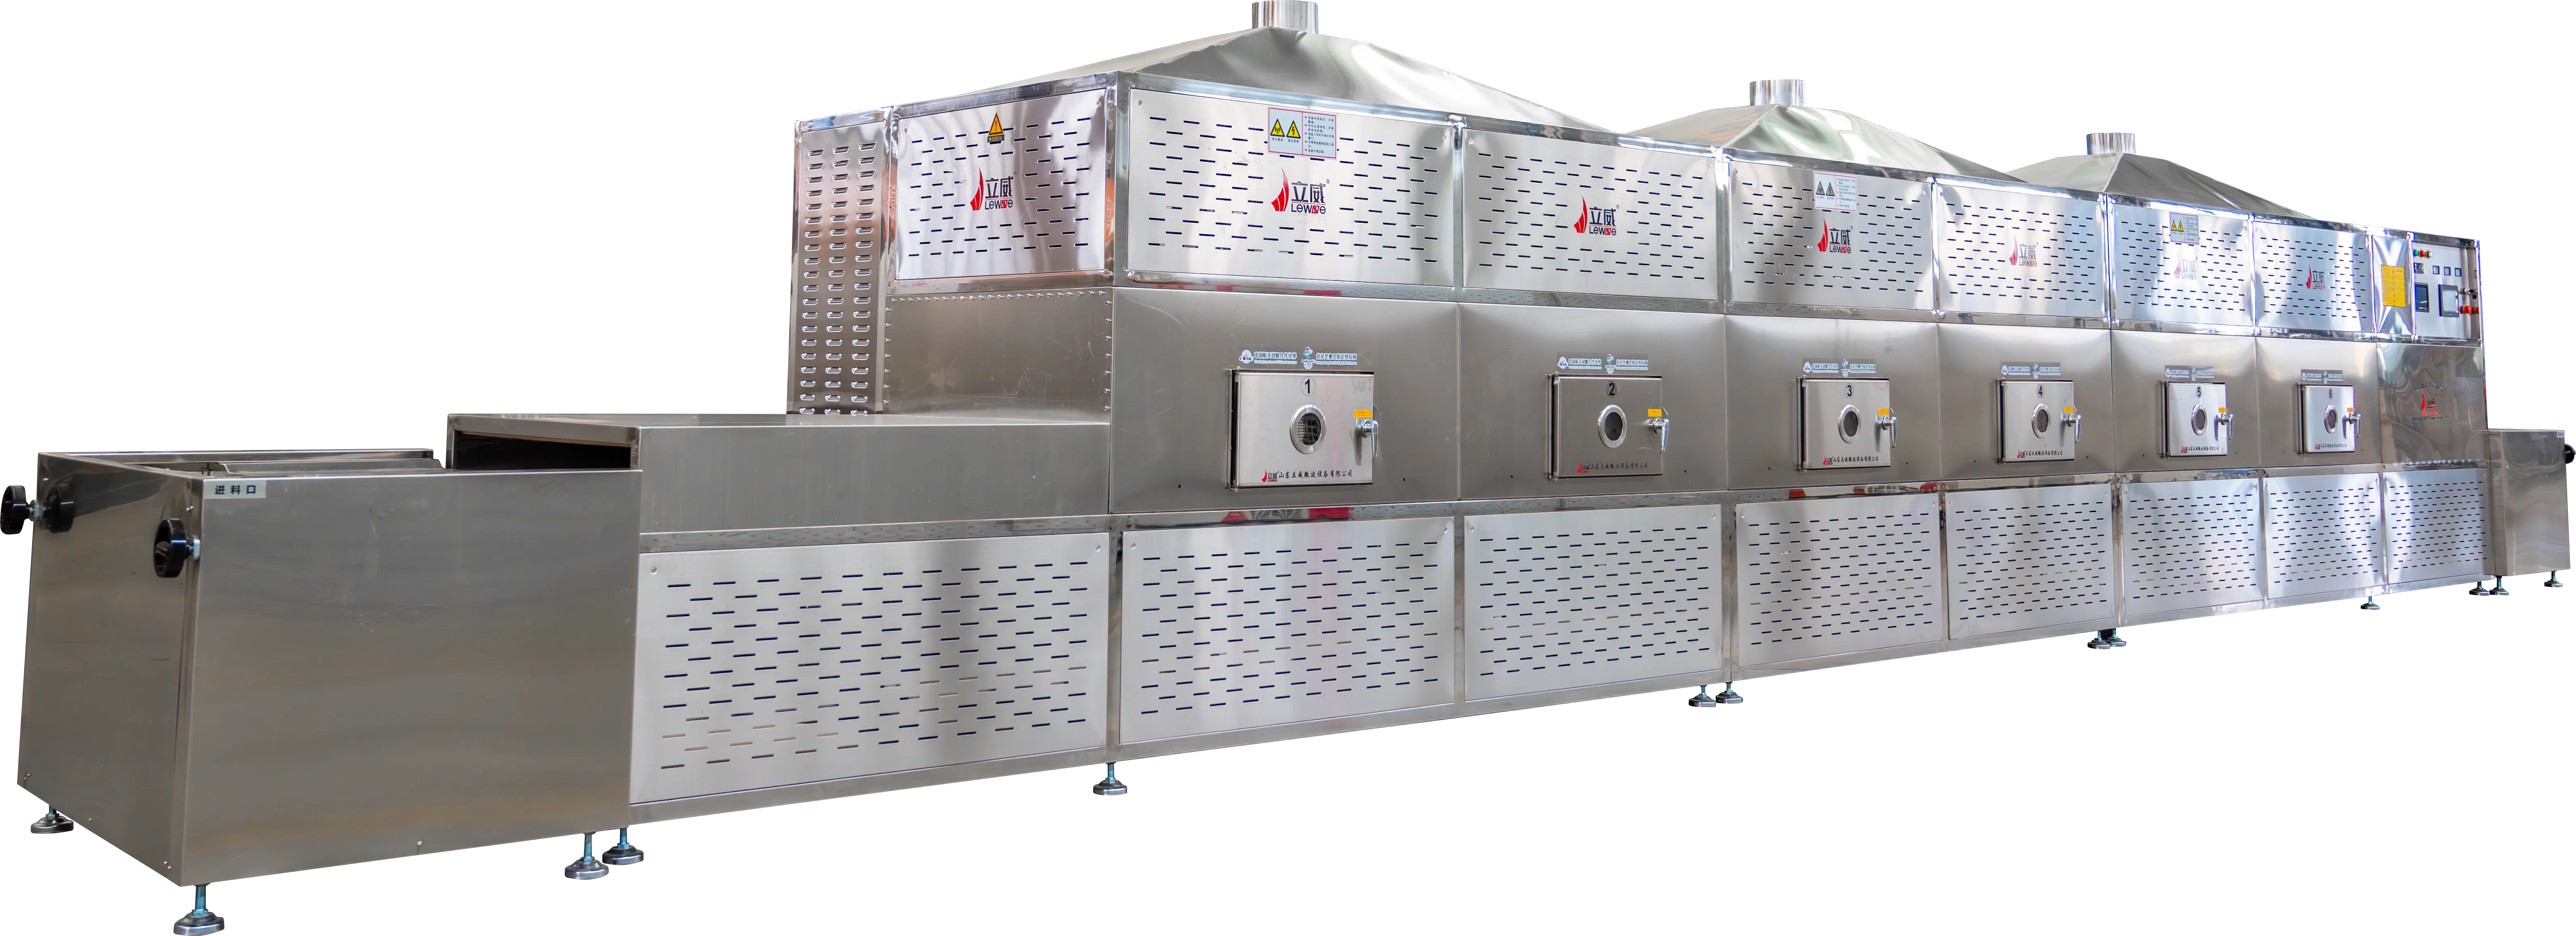
Our 60 kW industrial tunnel type microwave dryer adopts 2450 MHz microwave technology. Microwave energy acts on polar water molecules inside raw materials, making molecules vibrate and rub at high frequency to generate heat. With multi-cascaded heating chambers and adjustable total 60 kW microwave output, the equipment delivers stable continuous volumetric heating from inside out. Materials are transported by conveyor belt through the tunnel cavity. Internal moisture evaporates quickly under microwave action, and water vapor is exhausted by the dehumidification system to complete uniform dehydration. Synchronously, microwave electromagnetic fields realize in-situ sterilization. This tunnel dryer fits medium and large production lines for continuous drying and sterilization of diverse raw materials.
Core Strengths
High efficiency and energy saving to cut running cost: This 60 kW tunnel microwave dryer uses internal penetrating heating, lowering energy consumption by 30%-50% and shortening drying time greatly compared with hot air drying, with high thermal conversion efficiency.
Uniform heating to guarantee stable product quality: Slot-antenna feeding creates even microwave distribution inside the cavity. Inside-out heating prevents over-dried surfaces and wet cores, and low processing temperature protects active components.
Intelligent control system for easy operation: PLC touch screen supports preset process curves, stepless power adjustment and variable conveyor speed. Imported infrared sensors keep temperature fluctuation within 3 °C for precise parameter control.
One-step drying and sterilization to enhance hygiene: Microwave thermal and biological effects deactivate microorganisms during dehydration. Fully automatic continuous processing effectively avoids secondary contamination.
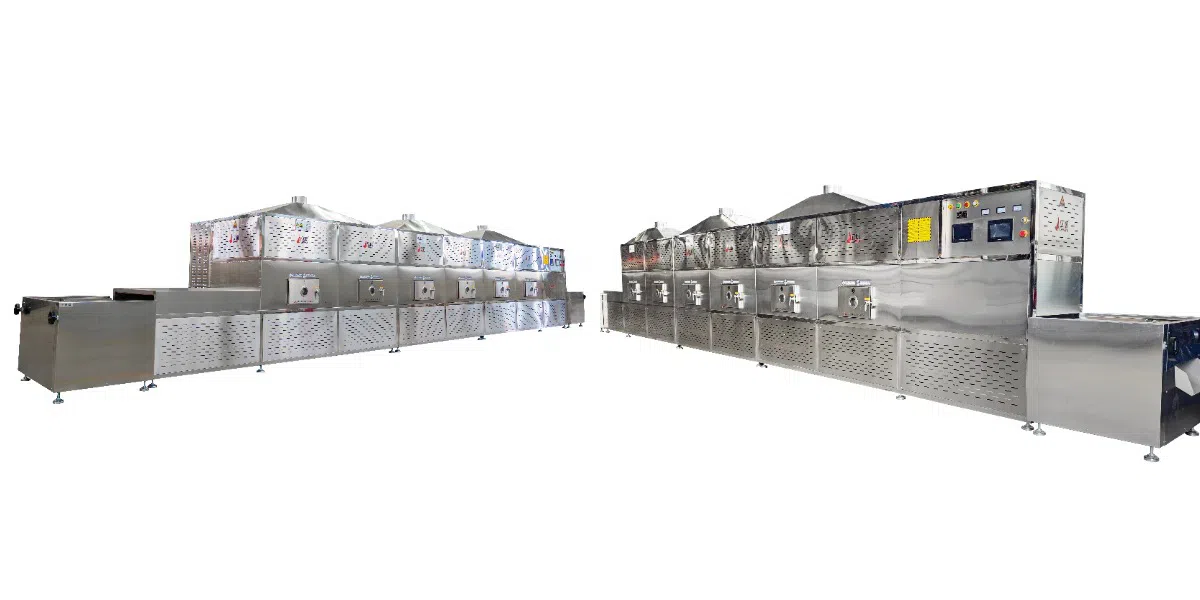
Continuous assembly line production with small footprint: The tunnel conveyor design enables automatic feeding and discharging for large throughput. Custom wider belts and higher-capacity versions can be customized according to production demands.
Safe and eco-friendly design that meets industry standards: Built-in suppressors limit microwave leakage within safety limits. 304 stainless steel contact parts satisfy GMP standards, and modular structure enables easy cleaning without dust pollution.
FAQ
What materials can this 60 kW tunnel microwave dryer process?
This dryer is widely applicable for food raw materials, starch, spice powder, plant extracts, chemical filter cakes, mineral powders and other solid materials requiring drying and mild sterilization.
Is the microwave power adjustable?
Yes. The total 60 kW microwave power supports segmented stepless adjustment, and conveyor speed can also be regulated by frequency converter to fit different moisture requirements.
How about the microwave leakage of the machine?
Microwave suppressors are installed at the inlet and outlet. Standard version leakage ≤5 mW/cm², optional upgraded version reaches ≤1 mW/cm², complying with relevant industrial safety standards.
Can the equipment meet pharmaceutical GMP requirements?
Yes. The material contact parts adopt 304 stainless steel, the whole structure is easy to disassemble and clean, which meets GMP hygiene requirements for pharmaceutical and high-grade food production.
Can we customize the machine specification?
Customization is supported. We can adjust belt width, cavity length and increase power configuration according to customer’s required throughput and material characteristics.
What is the main difference between microwave drying and hot air drying?
Microwave heats from inside the material, faster and more uniform. It saves energy, avoids surface crusting, and can complete sterilization together with drying, while hot air relies on slow external heat conduction.