
Product Description
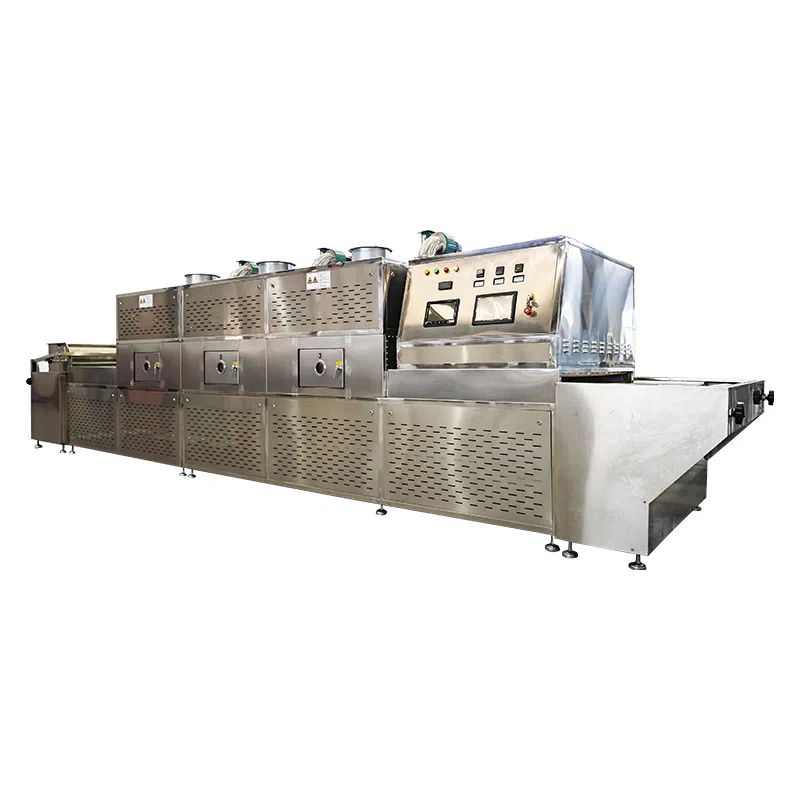
This continuous conveyor tunnel Plant Microwave Enzyme Deactivating Equipment is engineered for inline enzyme passivation of freshly harvested botanical feedstock. Fresh plant tissues naturally contain endogenous oxidase groups. Without timely passivation, these active enzymes trigger oxidative browning, decompose precious bioactive compounds and impair unique aroma during subsequent drying, packaging and storage. This Plant Microwave Enzyme Deactivating Equipment provides a dry thermal alternative to traditional hot-water or steam blanching, realizing rapid enzyme suppression across a diverse portfolio of fresh botanical raw materials.
Microwave dielectric energy penetrates multi-layer plant tissue and agitates intracellular polar water molecules to generate rapid frictional heat originating inside the plant matrix. Fresh plant stock is spread into regulated thin layers on hygienic food-grade conveyor belts and passes through segmented microwave treatment zones under variable conveying speed control. Built-in vapour evacuation ducts instantly extract moisture released from succulent plant cells. The integrated continuous workflow completes targeted enzyme inactivation together with mild pre-dehydration within a single pass on this Plant Microwave Enzyme Deactivating Equipment.
Core Strengths
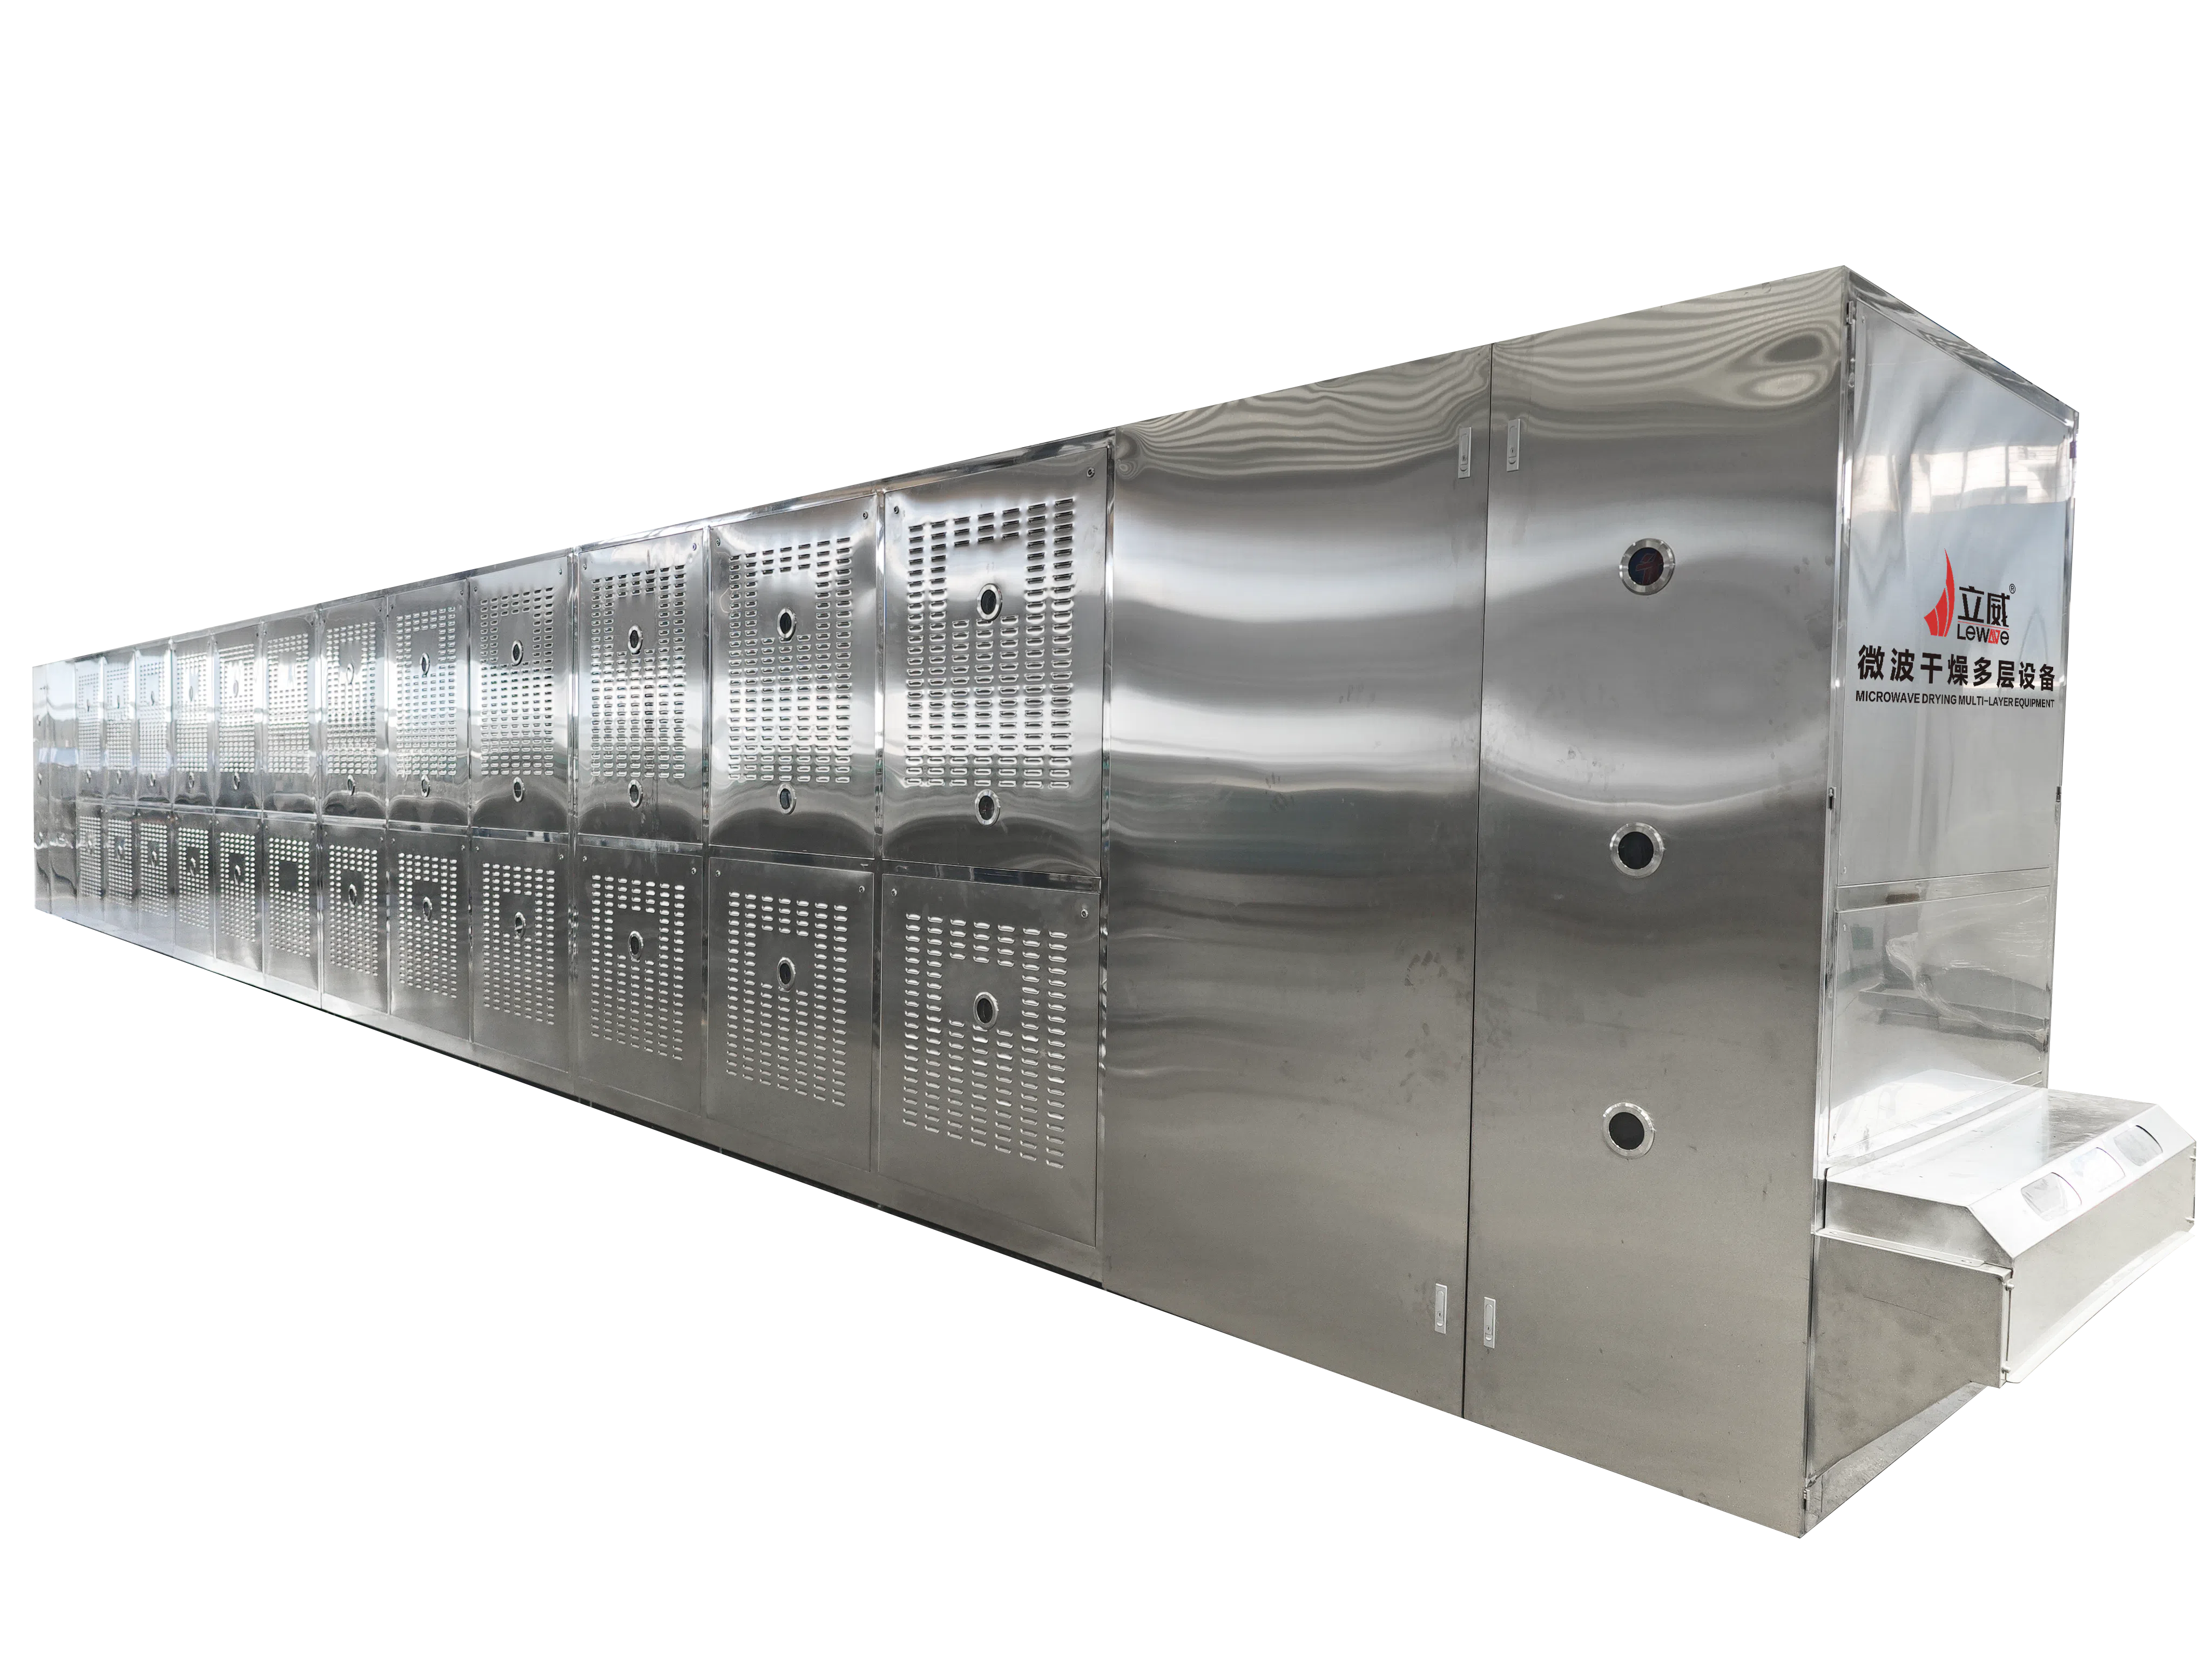
Uniform in-tissue dielectric heating delivers consistent enzyme passivation throughout plant sections. It effectively restrains enzymatic browning reactions and preserves the native colour, aromatic profile and heat-sensitive bioactives of fresh plant feedstock processed by this Plant Microwave Enzyme Deactivating Equipment.
Dry heating mode removes the risk of nutrient leaching inherent in immersion blanching workflows. It avoids tissue softening, pulping and structural collapse, keeping the complete morphological integrity of botanical raw materials treated on the Plant Microwave Enzyme Deactivating Equipment.
Dynamic PLC parameter tuning adapts to fresh foliage, flowers, rhizomes and other plant materials with divergent thickness and inherent moisture. Smooth food-grade contact surfaces simplify recurring sanitation cycles for production lines fitted with Plant Microwave Enzyme Deactivating Equipment.
Fully enclosed microwave containment cabins comply with global industrial safety specifications. Uninterrupted inline operation lifts hourly processing capacity. Plant materials processed by the Plant Microwave Enzyme Deactivating Equipment become premium starting materials for herbal tea blending, plant extraction and dehydrated vegetable manufacturing.
Equipment Composition
The plant microwave enzyme deactivating equipment adopts fully automatic tunnel type assembly line structure with food grade anti pollution modular design. It runs reliably under continuous working conditions and meets food and herbal hygiene standards. The complete set includes feeding unit, even material spreading section, multi cavity microwave enzyme deactivating tunnel, exhaust dehumidification system, online temperature monitoring, PLC intelligent control cabinet and automatic discharging unit. It is designed for large scale standardized continuous enzyme deactivation of various fresh plant raw materials.
Application Fields
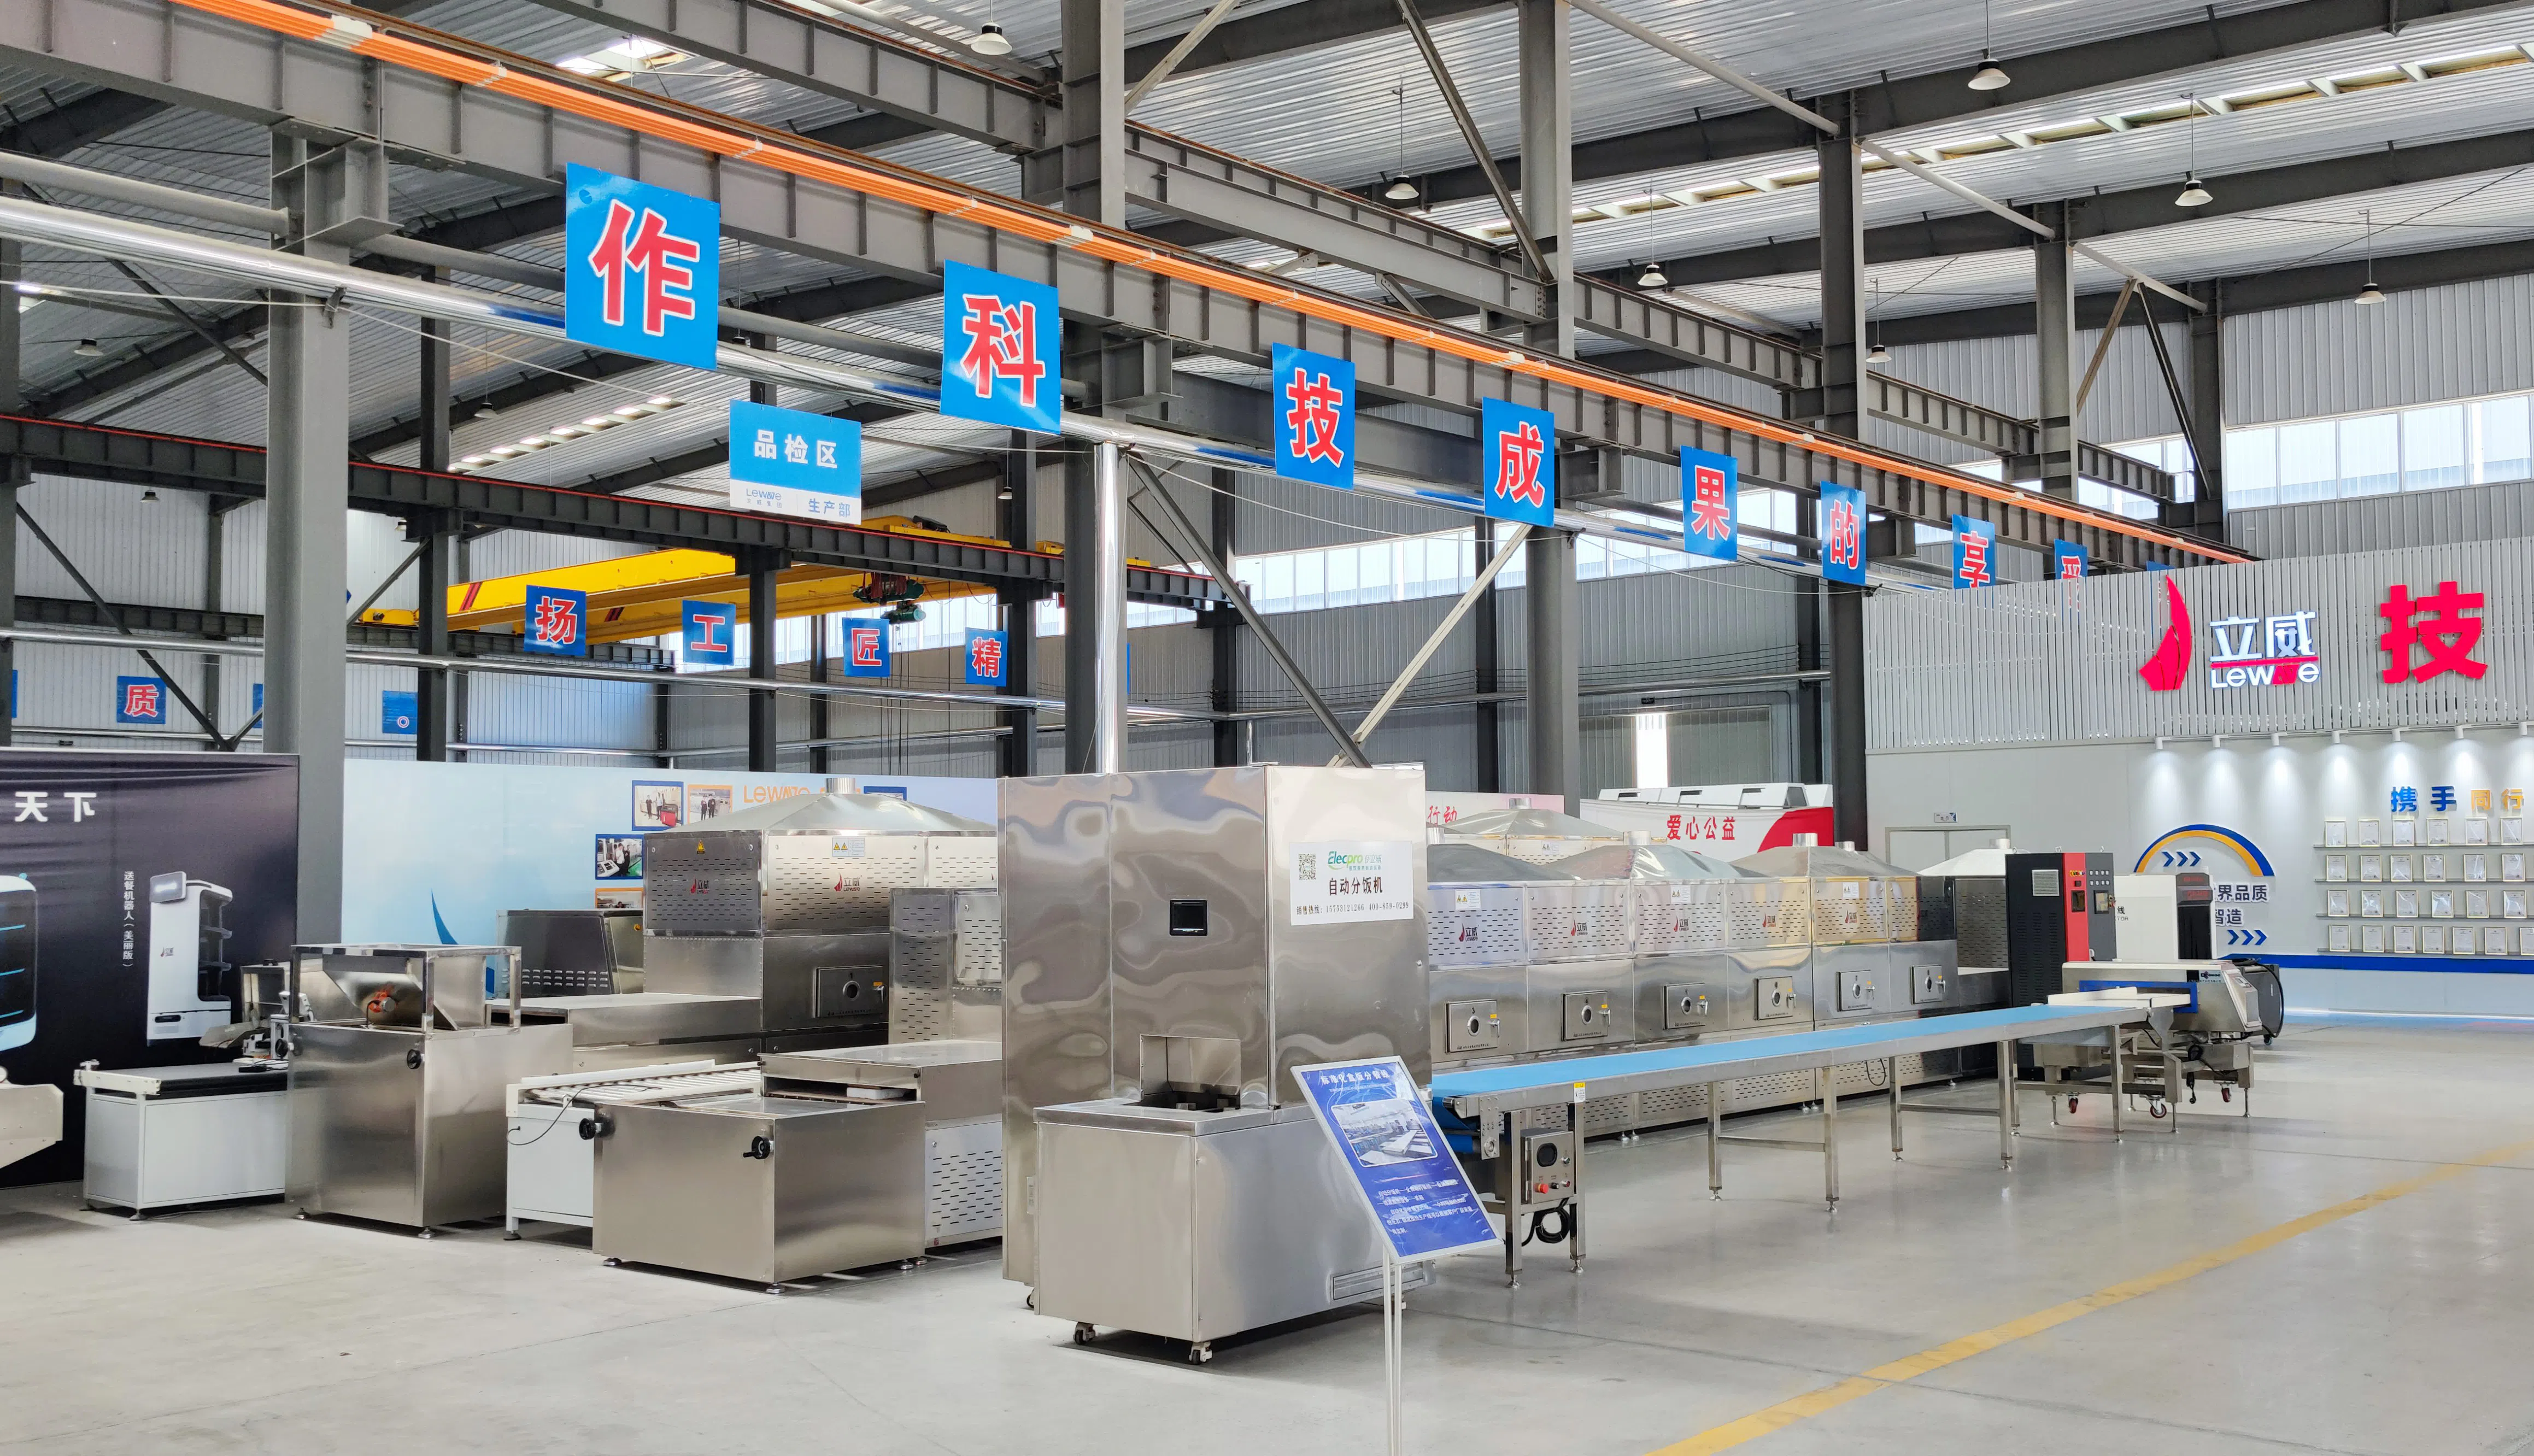
Custom developed for herbal processing factories, plant extract enterprises, edible flower and vegetable processing plants and export manufacturers. It is widely used for continuous microwave enzyme deactivation, pre dehydration and color protection of fresh plant raw materials. The treated materials maintain natural color, intact shape and rich active ingredients.

