
Product Description
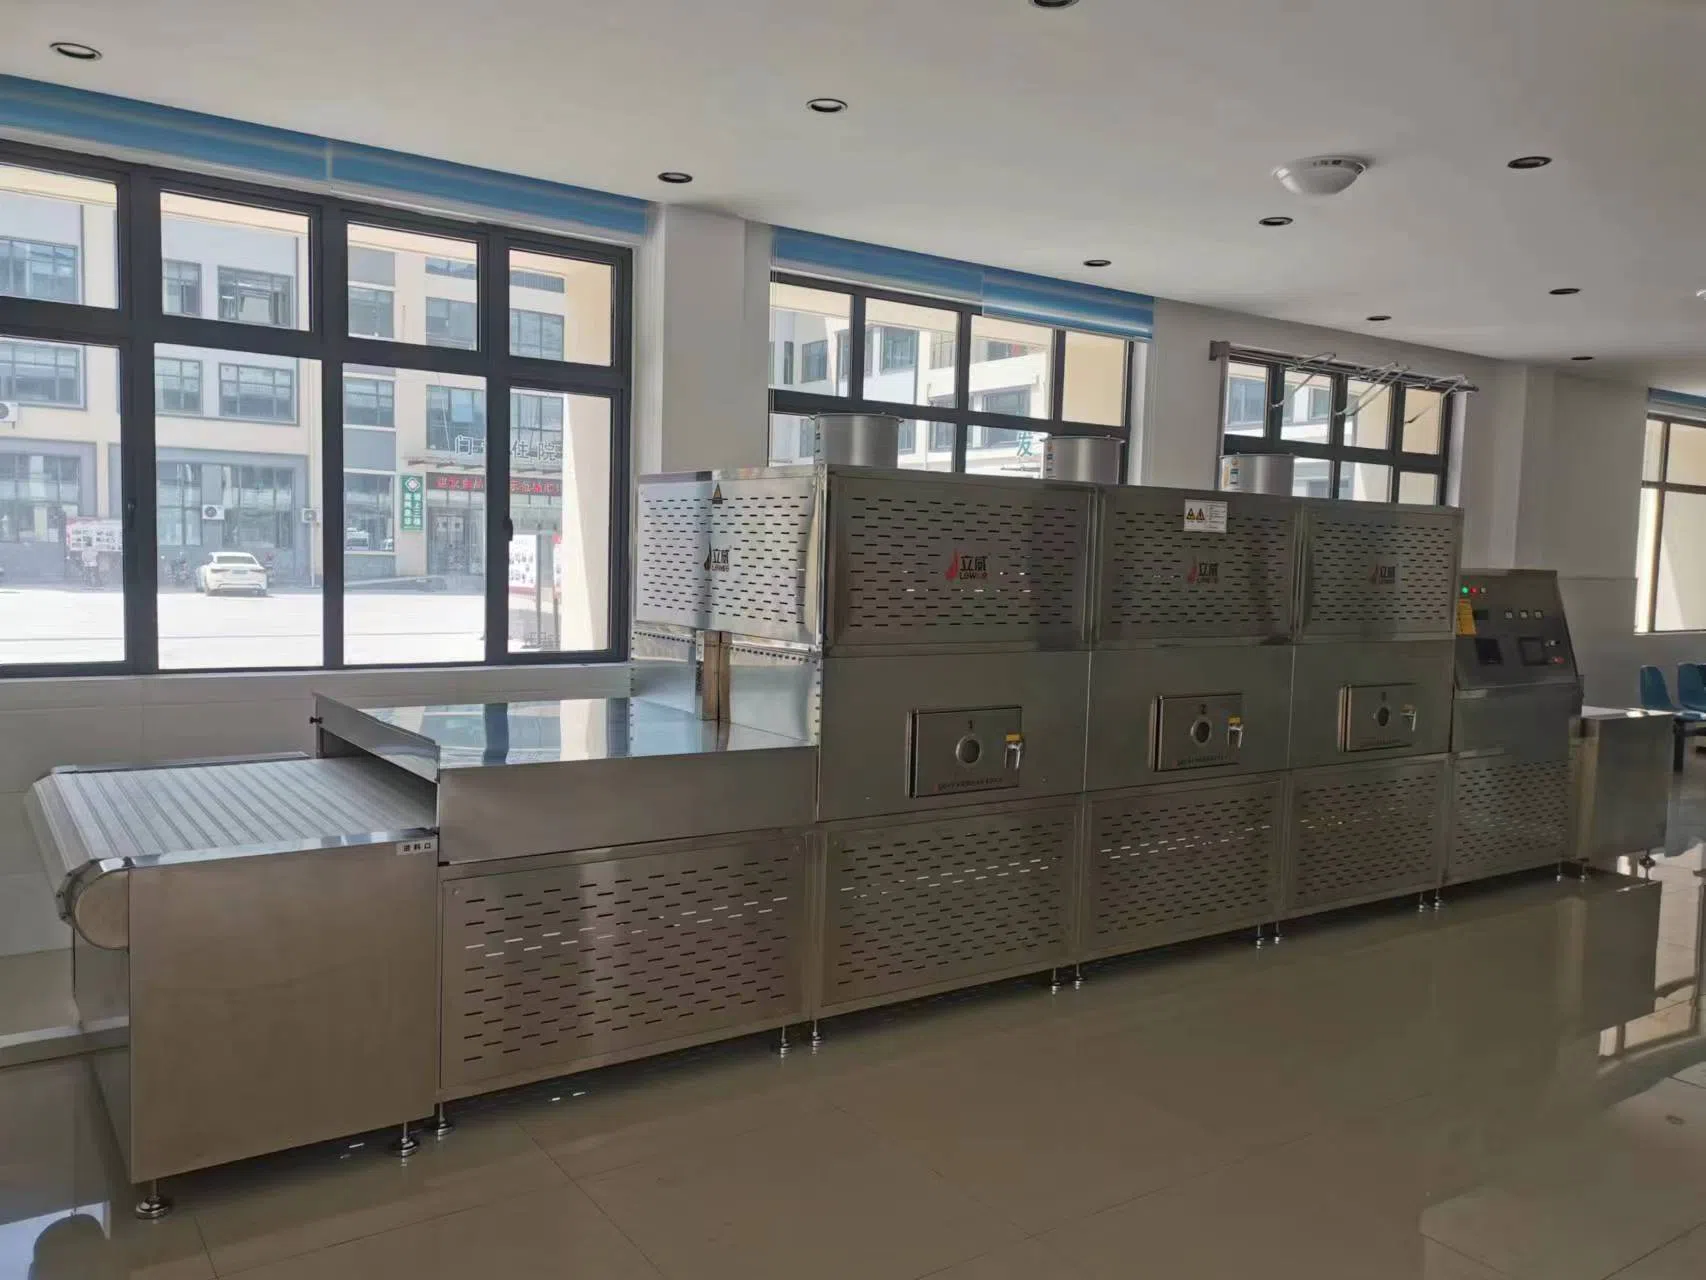
The Industrial Microwave Box Meal Reheater utilizes a high-energy microwave electromagnetic field to act directly on polar molecules such as water and protein inside boxed meals. These molecules vibrate, rub and collide at an ultra-high frequency of 2.45 billion times per second, quickly converting electromagnetic energy into thermal energy. Featuring unique microwave penetrating heating technology, the machine achieves synchronous and uniform heating of the entire box meal. It thoroughly solves the common industry pain points of traditional hot air and steamer heating, including uneven internal and external temperature, slow heating, inconsistent dry-wet state and deteriorated food taste.
During operation, boxed fast food and bento meals are stably conveyed into the multi-chamber series microwave heating channel through a variable-frequency speed-regulating conveyor belt for full-angle penetrating heating. The equipment rapidly raises the overall temperature of meals, while the independent dehumidification and heat exhaust system timely discharges residual water vapor and waste heat. This effectively avoids moisture accumulation, mushy food and back dampness of meals. While realizing fast reheating, the machine eliminates bacteria and microorganisms via microwave biological effects. It achieves integrated functions of rapid reheating, fresh-keeping and bacteriostasis, ensuring stable meal temperature, consistent taste and edible safety.
Main Advantages
1. High Energy‑Efficiency, Lower Group‑Meal Reheating Costs
The box‑meal microwave heater adopts penetrating internal heating. Electromagnetic energy acts directly on water molecules in food and converts into heat. No pre‑heating or hot‑air conduction is required, enabling simultaneous heating from inside to outside. Compared with traditional steam ovens, hot‑air ovens and gas‑fired heaters, microwave reheating saves 30%‑50% energy and cuts reheating time by 50%‑80%, with thermal efficiency above 70%. Low power consumption and fast temperature rise greatly reduce operational costs for central kitchens and group‑catering enterprises for mass reheating. It supports 24‑hour continuous large‑scale production.
2. Thorough & Even Heating, Preserving Food Taste & Appearance
Optimized microwave feeding technology ensures even and stable microwave distribution inside the cavity. It eliminates typical defects of conventional heating: hot surface yet cold core, uneven temperature, dried‑out surface, undercooked interior and diluted soup. Thanks to microwave penetration, each boxed meal is reheated gently and uniformly. Original flavour, colour and moist texture are well retained, avoiding mushy, dry, clumpy or off‑taste food. Consistent temperature and good appearance across every batch improve output quality and end‑user dining experience.
3. Smart Precise Control for All Types of Group Meals
Equipped with PLC touch‑screen control system, the unit can set and store multiple custom reheating profiles for box meals and pre‑cooked food. Microwave power is stepless adjustable in sections, and conveyor speed is frequency‑convertible. Reheating temperature and duration can be precisely matched for rice, noodles, meat‑vegetable combos and pre‑made bento boxes. High‑precision infrared temperature sensor keeps temperature fluctuation ≤3℃. Saved parameters can be recalled with one‑click for accurate replication, ensuring consistent quality across different food types in mass production.
4. Simultaneous Reheating & Sterilization, Meeting Export‑Grade Food Safety Standards
While reheating box meals rapidly, microwave thermal and biological effects kill harmful micro‑organisms such as E. coli, Salmonella and mould, restraining bacterial growth and solving excessive bacteria risks for cooled pre‑cooked and delivered meals. Fully enclosed automatic production line avoids human contact with food and secondary contamination, extending shelf‑life. Hygiene performance complies with international GMP and FDA standards, suitable for premium group catering and export‑oriented pre‑cooked food processing.
5. Continuous Production Line Operation, High Capacity with Small Footprint
The fully‑automatic tunnel‑type conveyor enables non‑stop 24‑hour reheating. Feeding, heating, dehumidification and discharging run automatically without manual arranging, re‑heating or on‑site attendance. Modular compact design occupies less floor space and delivers higher efficiency than traditional batch‑mode standalone heaters. Production lines with custom width, length and power are available to satisfy mass standardized production for small‑to‑medium central kitchens and large group‑meal distributors.
6. Safe, Clean & Eco‑Friendly for Food‑Workshop Conditions
Multi‑stage microwave suppressors are installed at inlet and outlet to keep microwave leakage within national safety limits for stable and safe operation. All food‑contact parts are made of 304 food‑grade stainless steel, anti‑corrosion, easy‑to‑clean and free of sanitary dead corners to meet food‑workshop hygiene requirements. Closed low‑temperature reheating generates no flue gas, oil fume or residues. Environment‑friendly and compliant with safety specifications for domestic and overseas central kitchens and pre‑cooked food factories.
Equipment Composition
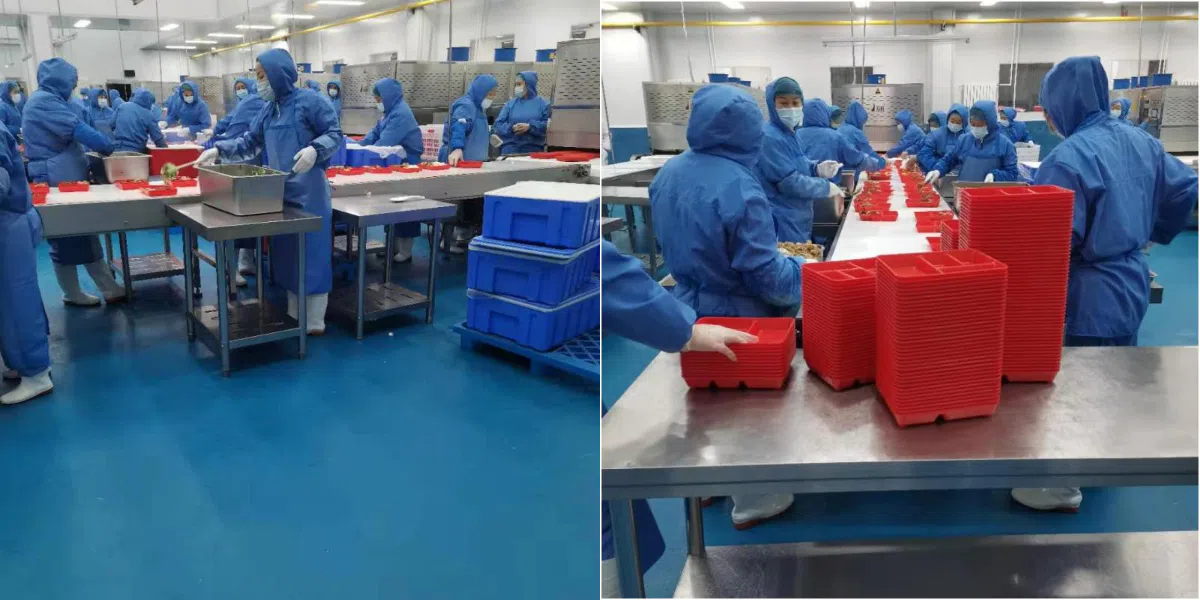
The box‑meal microwave reheater features a fully‑automatic tunnel‑type continuous assembly‑line structure. Designed with full food‑grade cleanliness, it delivers stable operation, low noise and easy cleaning & maintenance. The complete unit consists of six core systems, well‑suited for large‑scale and standardized production of box‑meal heating, reheating and sterilization in central kitchens, fast‑food factories and group‑catering enterprises.
| Component | Function Description |
|---|---|
| Microwave Generating System | It is the core energy‑generating unit of the equipment. Equipped with high‑stability industrial magnetrons, it outputs even and stable microwave energy with low loss. The microwave power can be precisely adjusted according to box‑meal specifications, loading weight and initial temperature. It adapts to gentle and fast reheating processes for various fast‑food and bento meals and avoids local overheating or dried‑out hard food. |
| Microwave Heating Cavity | It is a dedicated closed heating cavity for box meals, optimized via electromagnetic field simulation. Microwave is evenly distributed inside without blind spots. The cavity adopts rounded‑corner dust‑free clean structure, which resists oil and dirt accumulation. Suitable for continuous mass reheating of boxed fast food, it guarantees uniform heating, good appearance and eliminates temperature stratification for every box meal. |
| Material Conveying System | It adopts food‑grade high‑temperature‑resistant anti‑slip mesh belt or flat belt, featuring stable running, low noise and shock resistance. It effectively prevents box‑meal shifting, tipping and spillage. Equipped with variable‑frequency motor, the conveying speed can be adjusted freely according to production capacity and reheating time for uninterrupted mass reheating on assembly lines. |
| Microwave Suppression System | Multiple high‑efficiency microwave suppressors are installed at inlet and outlet with professional shielding‑sealing structure to block microwave leakage. Microwave leakage is far below international safety standards. The equipment operates safely and compliantly for long‑term continuous production in food workshops. |
| Moisture‑Heat Exhaust System | Fitted with intelligent constant‑temperature ventilation and dehumidification‑heat‑dissipation devices, it timely discharges hot air and water vapor generated during reheating. It prevents condensed water dripping inside the cavity, avoids soggy meals and diluted soup, and maintains good texture and appearance of finished meals. |
| Automatic Control System | Full‑automatic PLC touch‑screen control for simple and intuitive operation. Multiple sets of dedicated reheating parameters for box meals and fast food can be preset and stored. Stepless adjustable microwave power, running speed, heating temperature and air‑vent volume deliver precise temperature control and repeatable processes. Fully automatic operation without manual attendance, suitable for standardized mass production of group meals. |
Application Fields
The Industrial Microwave Box Meal Reheater is specially developed for industrial‑scale reheating and sterilization of group‑catering food. It is widely used for rapid heating, constant‑temperature reheating, sterilization and fresh‑keeping of various boxed fast‑food, bento meals, nutritious meals and pre‑cooked meals. Treated food features even temperature, original flavour and qualified microbial indicators. It applies to central kitchens, group‑meal distributors, airline catering, high‑speed‑rail catering, school meals and food export processing. Its key application categories are listed below:
Reheating & Sterilization for Boxed Fast‑food
Mass rapid reheating for Chinese fast food, bento boxes, rice with toppings and set‑meal boxes. It solves problems such as post‑delivery temperature drop, large temperature difference and bacterial growth, and realizes consistent serving temperature and product quality.
Heating for Pre‑cooked & Convenience Meals
Industrial standardized heating and sterilization for room‑temperature pre‑cooked dishes, vacuum‑packed meals, instant nutritious meals and quick‑serve bentos. Suitable for assembly‑line mass production of pre‑made food.
Special Heating for Transportation Catering
Centralized reheating and sterilization for airline meals, high‑speed‑rail meals, EMU meals and cruise ship food. Fast reheating keeps meal boxes intact without damage and meets food safety standards for premium catering services.
Heating for Group Nutritious Meals
Large‑volume continuous reheating for school nutritious meals, corporate group meals, hospital catering and construction‑site collective meals. It improves serving efficiency and guarantees food hygiene, complying with GMP and FDA international sanitary specifications for food export.

