
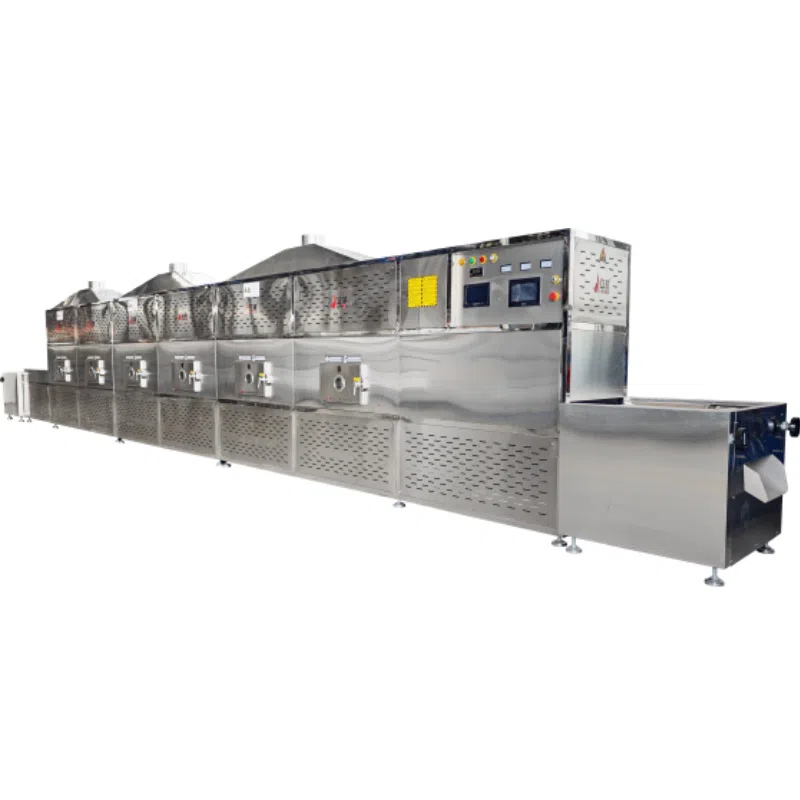
Product Description
Tunnel microwave heating equipment uses 2450 MHz microwaves to penetrate into materials and interact with internal polar molecules such as water molecules. Upon absorbing microwave energy, polar molecules execute polar rotation following the electric‑field frequency. Intense intermolecular collisions produce massive frictional heat, so every part of the material gains heat and rises in temperature simultaneously.
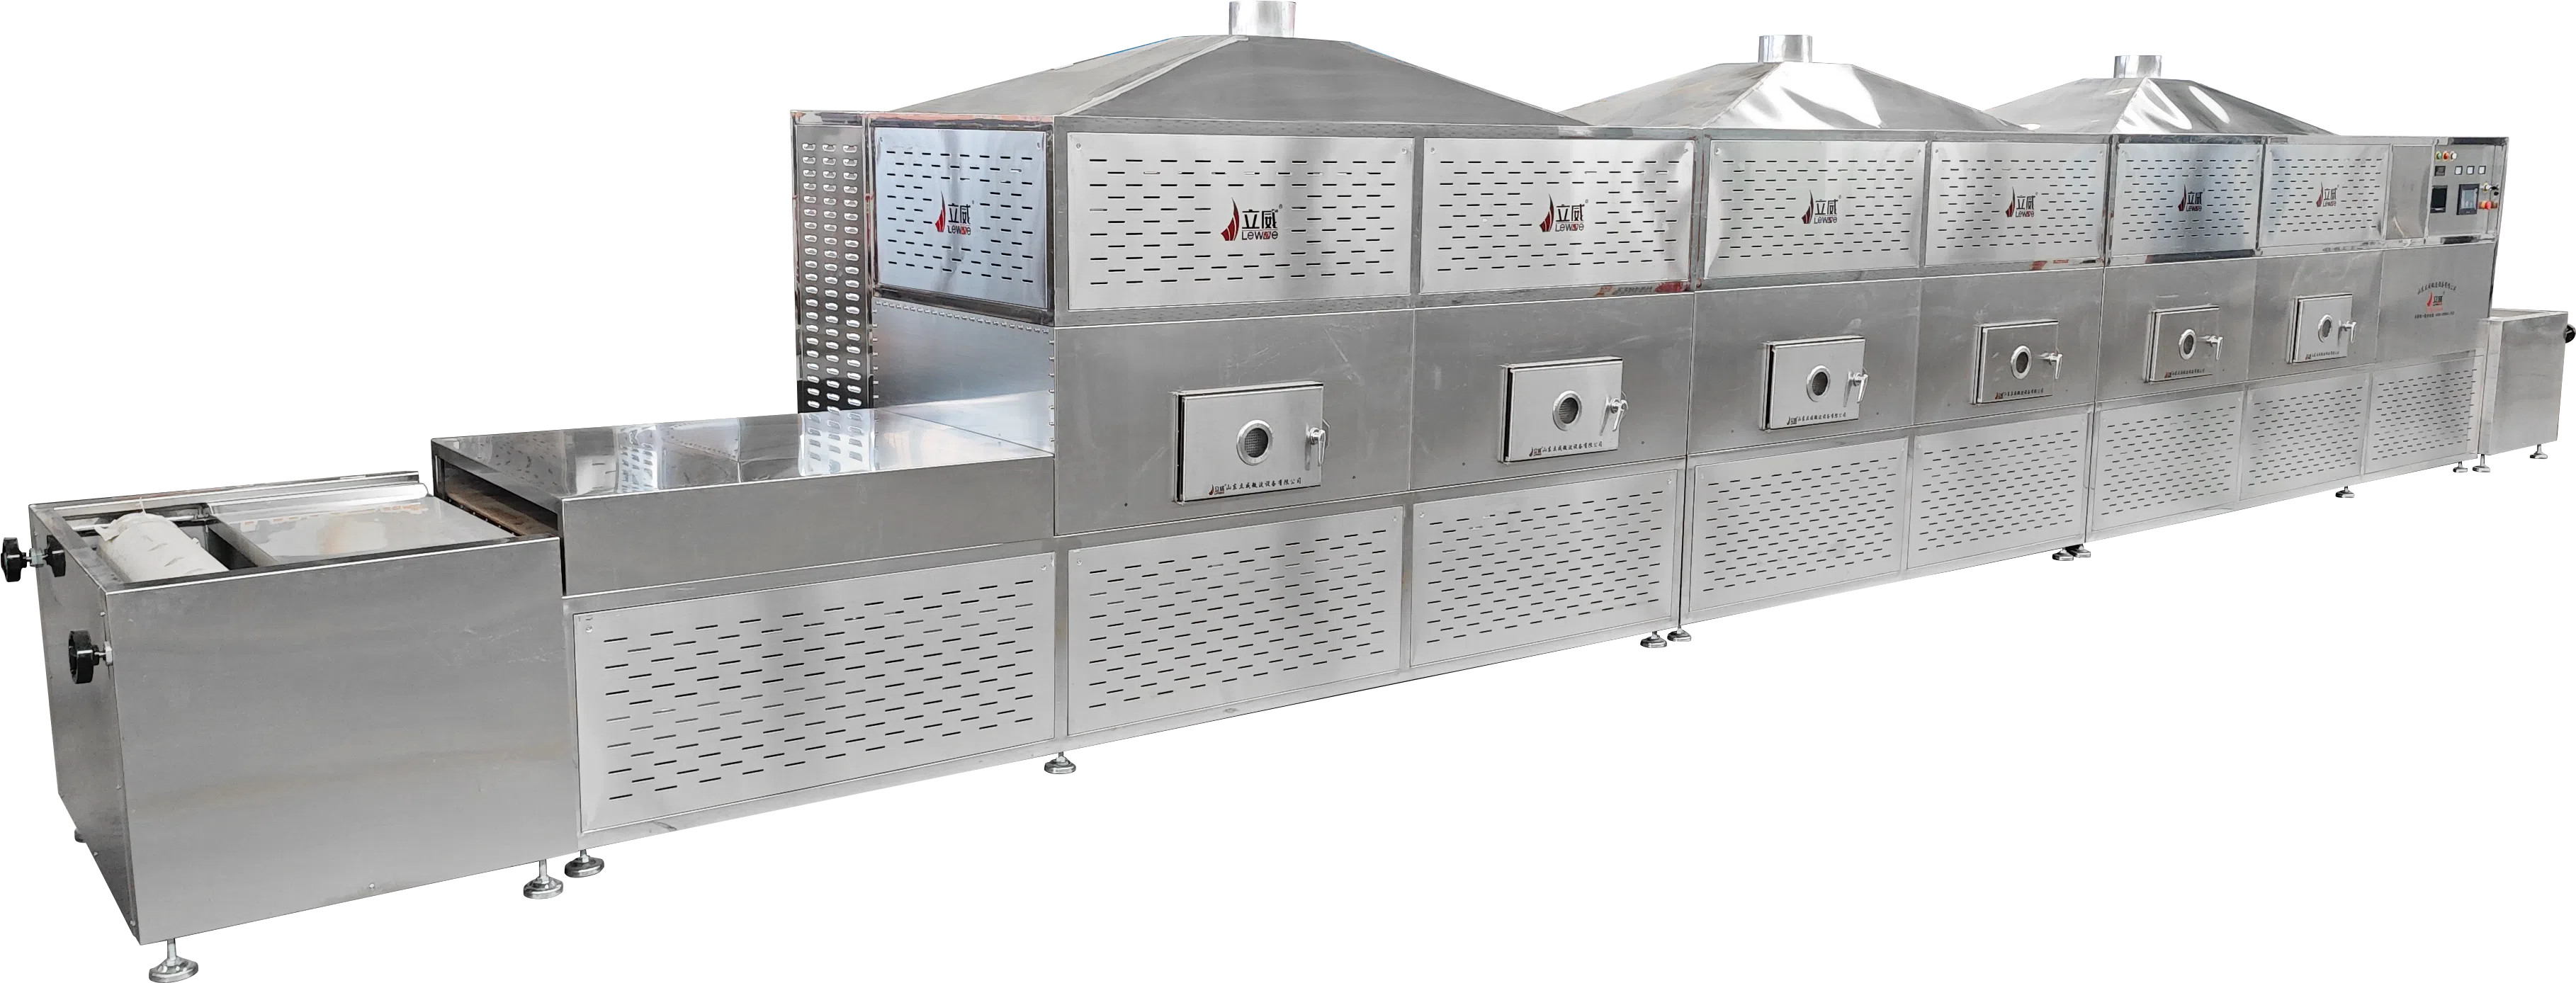
Materials are transported by conveyor belt into the tunnel channel composed of multiple connected microwave heating cabinets. Fast and uniform heating is realized as materials continuously travel through the microwave field.
Main Advantages
Fast Heating Speed & Greatly‑Improved Production Efficiency
Microwave heating is an internal volumetric heating method. Electromagnetic energy directly acts on polar molecules (e.g. water molecules) inside materials, causing them to vibrate and rub at 2.45 billion times per second to generate heat. Materials are heated simultaneously from inside out without relying on heat conduction. Microwaves can penetrate up to 5 cm into materials. Its heating speed is 4‑10 times faster than conventional methods, and satisfactory heating results can usually be achieved within tens of seconds to several minutes. Featuring a continuous assembly‑line working mode, the equipment supports 24‑hour non‑stop production to meet large‑scale processing requirements.
Uniform Heating for Consistent Product Quality
As volumetric heating within dielectrics, microwave heating can theoretically achieve “gradient‑free heating” with barely any heat conduction inside the material. Materials keep moving through the tunnel and repeatedly pass through microwave peaks and troughs, which statistically improves heating uniformity. Traditional heating transfers heat from the surface inward, leading to large internal‑external temperature differences and frequent under‑cooked interiors or burnt surfaces. By contrast, microwave heating enables the inner and outer portions of materials to reach target temperatures simultaneously for superior product consistency.
Energy‑Saving & Low Operating Cost
Microwave power conversion efficiency generally exceeds 70%. Microwaves act directly on processed materials instead of heating the chamber itself, avoiding extra heat loss. It delivers 30%‑50% energy savings compared with conventional heating solutions. No auxiliary facilities such as boilers or piping systems are required; the unit only needs water and power for operation, significantly cutting capital investment and operating expenses.
Intelligent Control & Easy Operation
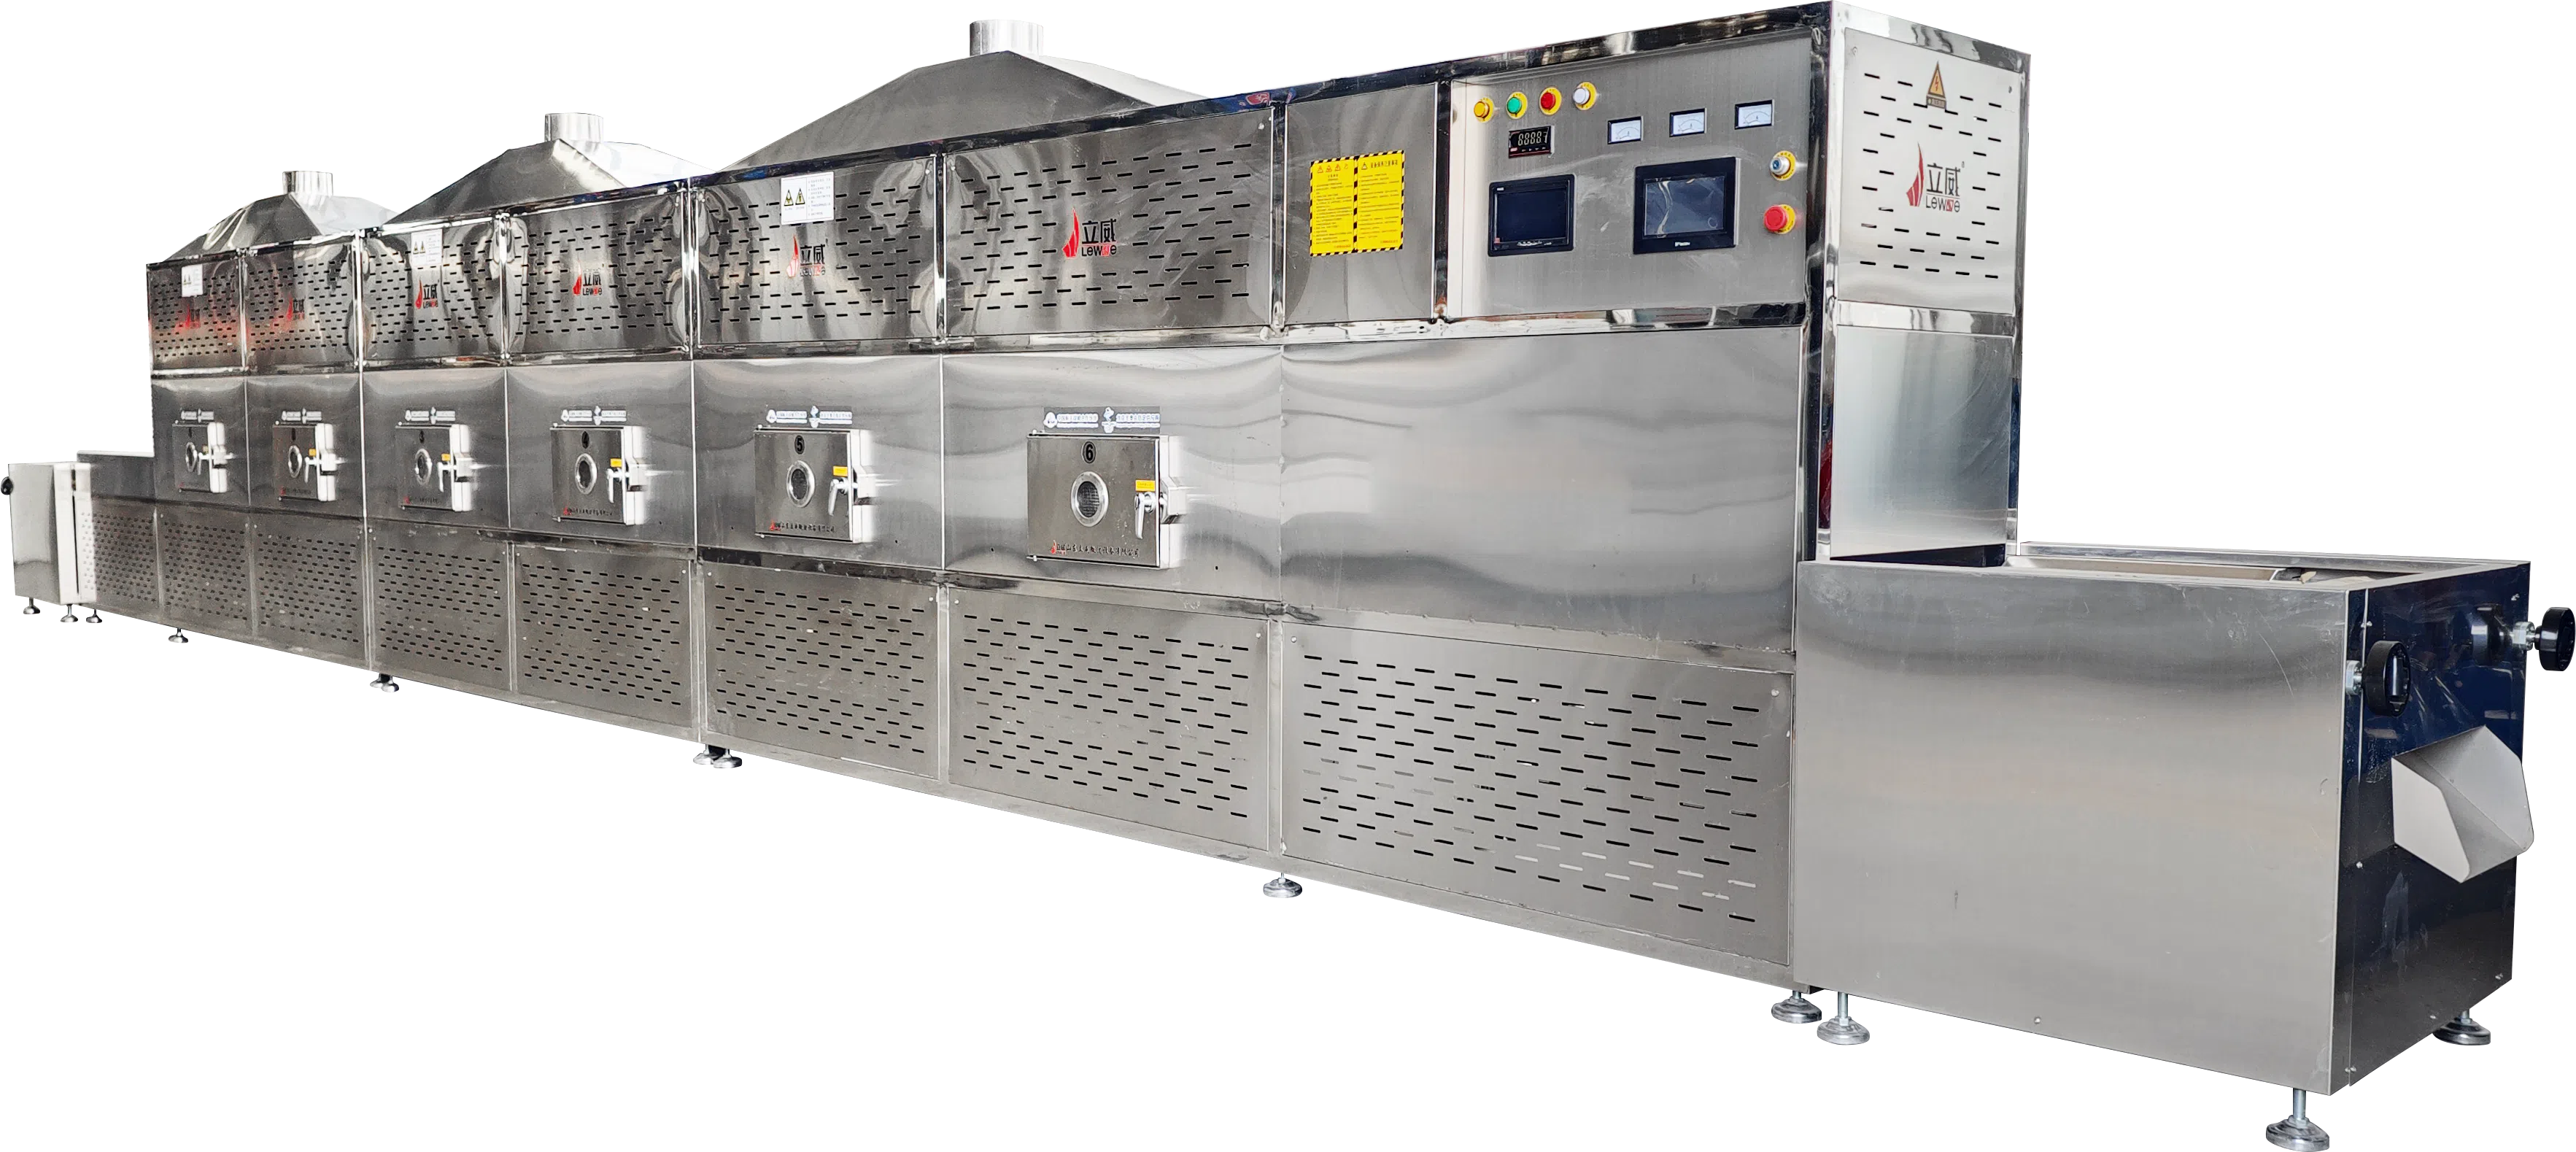
The whole machine adopts PLC programmable control with a touch‑screen HMI for simple, fast operation. Temperature, power and conveying speed are intelligently adjustable, while all operating parameters and working status are displayed in real time. Multi‑point temperature measurement and split‑section process control are supported, realizing closed‑loop regulation of temperature and power. Free of thermal inertia, microwave heating delivers precise temperature‑field control to satisfy refined requirements for diverse processes.
Safe & Eco‑Friendly for Better Working Conditions
The main body is integrally welded from 304 stainless steel for high durability. Microwave‑leakage suppression structures are installed at inlet and outlet, keeping leakage below the standard threshold (<5 mW/cm²). There is nearly zero microwave leakage, no radioactive residue and no harmful gas emission. The equipment features low external heat dissipation and low noise. Since the unit itself generates no heat or thermal radiation, working conditions for operators are greatly improved.
Built‑in Sterilization for Enhanced Hygiene Safety
While rapidly raising material temperature, the thermal effect of microwaves effectively eliminates bacteria and microorganisms. Compared with conventional thermal sterilization, microwave sterilization achieves qualified disinfection results at lower temperatures within shorter time frames, preserving nutrients, original color and flavor of products.
Compact Footprint to Save Floor Space
The tunnel‑type microwave equipment features a compact structure. Auxiliary installations including boilers, pipelines and coal yards are unnecessary, and no special plant requirements are needed. It brings low‑cost investment and quick returns, and substantially saves workshop floor area versus traditional heating production lines.
Equipment Composition
Component | Function Description |
|---|---|
Microwave Generating System | Produces microwave energy; core components are industrial‑grade magnetrons |
Microwave Heating Cavity | Working zone for material microwave heating; multi‑cavity cascaded assembly structure |
Material Conveying System | High‑temperature resistant conveyor belt with variable‑frequency speed adjustment |
Microwave Suppressor | Blocks microwave leakage to ensure operator safety |
Heat Exhaust System | Removes excess heat and waste gas from cavities in real time |
Automatic Control System | PLC touch‑screen operation; closed‑loop control for temperature and power |
Application Fields
Widely applied for heating, drying, sterilization, pyrolysis and other processes in food, pharmaceutical, chemical, environmental protection and other industries.
Food Industry: Fast heating & reheating of boxed meals & fast food; thawing and heating of cold‑chain food; heating and sterilization for meat, bean products and seasonings; tea fixation; nut roasting, vegetable dehydration, etc.
Pharmaceutical Industry: Heating, drying and sterilization for herbal raw materials and Chinese medicine pills.
Chemical & Environmental Protection: High‑temperature heating, thermal desorption, pyrolysis; soil remediation and other environmental‑protection scenarios.
Others: Heat treatment for bamboo‑wood goods, heating of chemical products, etc.


