
Product Description
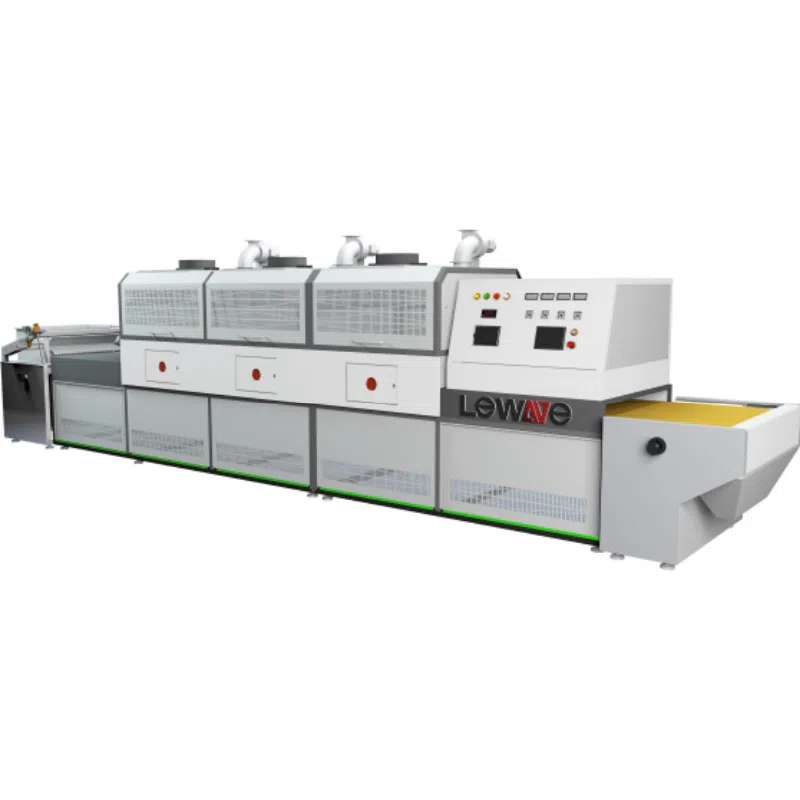
Microwave Grain Curing Equipment applies high‑frequency microwave energy directly to polar water molecules and organic molecules inside grains. These molecules vibrate, rub and collide at an ultra‑high rate of 2.45 billion cycles per second, swiftly converting electromagnetic microwave energy into thermal heat. Benefiting from microwave’s inherent penetrating heating capability, materials get heated uniformly from core to surface. This fundamentally avoids common flaws of conventional thermal machinery, such as undercooked interiors alongside over‑heated outer layers and uneven thermal distribution.
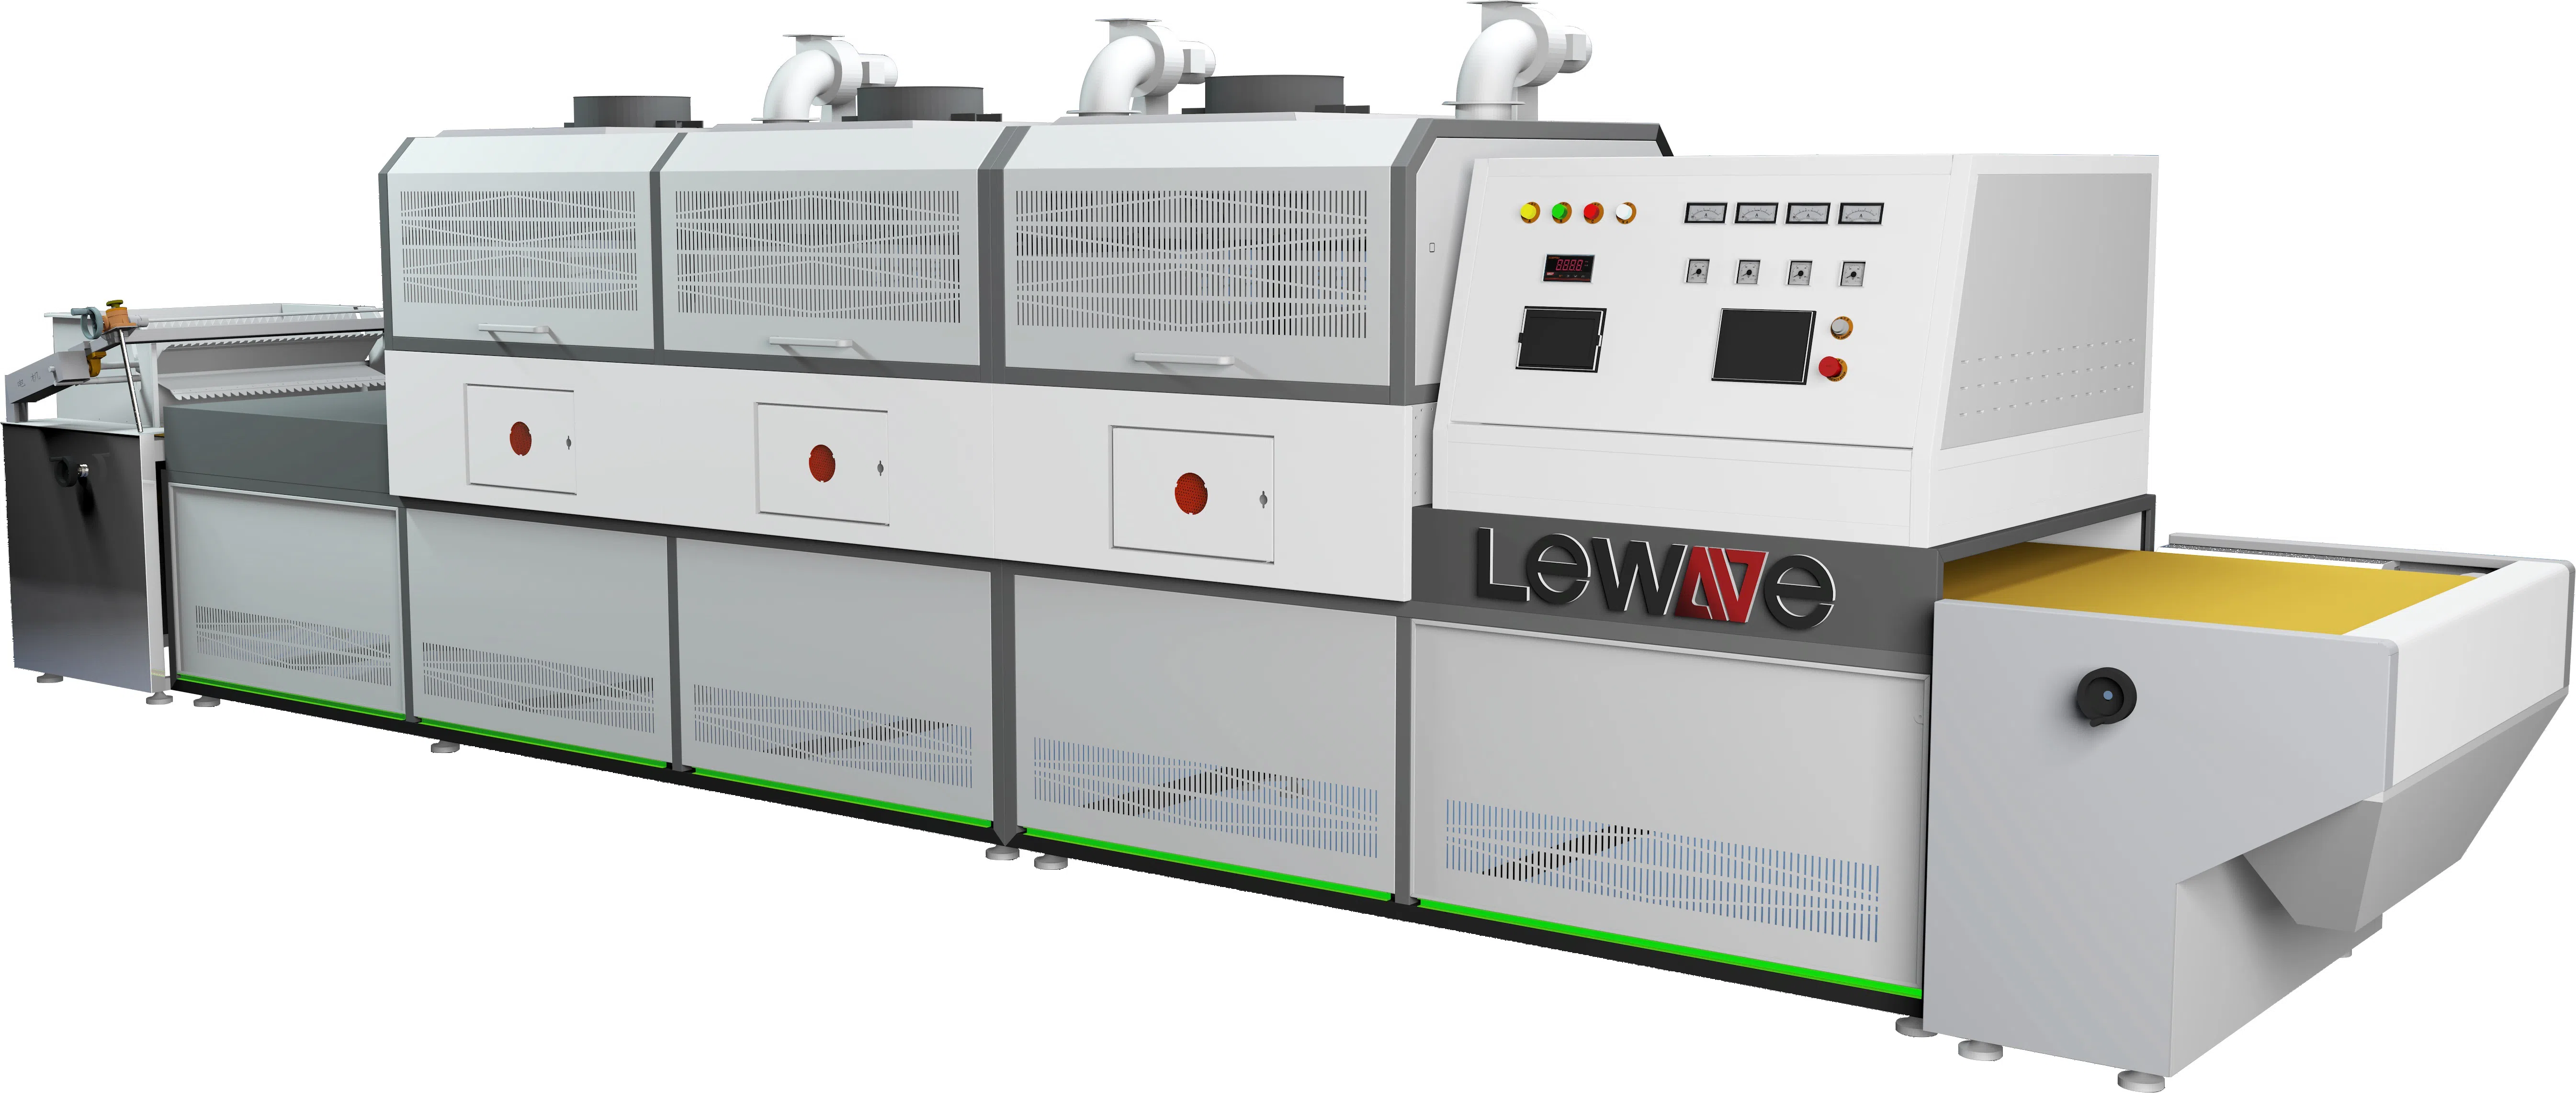
During operation, various whole‑grain raw materials are fed at steady speed by a variable‑frequency conveyor belt into a multi‑chamber cascaded microwave curing tunnel. Microwaves deliver full‑range penetrating heating across spread‑out materials. Grains rapidly reach target temperature to finish curing, puffing and aroma enhancement. Excess internal moisture vaporizes and is quickly evacuated by a dedicated moisture‑removal system, realizing one‑pass integrated processing of curing, drying and dehydration. Meanwhile, microwave electromagnetic fields damage the active structures of bacteria and insect eggs within materials to achieve simultaneous sterilization and mildew resistance, significantly extending the shelf‑life of finished grain products.
Main Advantages
Energy‑efficient Operation to Cut Multigrain Processing Expenses This microwave grain curing solution delivers volumetric internal heating. Electromagnetic energy is converted into heat directly within polar molecules of raw grains, achieving simultaneous heating throughout the material without hot‑air transfer or preheating. Compared with traditional drum‑roasting and hot‑air drying machinery, it realizes 30%‑50% energy savings and cuts processing duration by over 60%, with thermal conversion efficiency exceeding 75%. It consumes one‑third less energy than conventional grain roasters, lowering power expenditure for large‑batch curing and drying and suiting long‑term industrial‑scale production.
Uniform Stable Curing for Superior Grain Product Quality Optimized microwave energy‑feeding delivers even electromagnetic‑field distribution across the curing chamber with zero dead zones. It eliminates typical defects of conventional grain processing such as burnt outer layers with raw interiors, inconsistent curing levels, partial under‑done grains and uneven coloration. Penetrating low‑temperature heating enables synchronized curing, dehydration and aroma enhancement for cereals and beans. Dietary fiber, natural nutrients and intrinsic fragrance are well preserved. Finished grains feature bright appearance, crisp texture and consistent curing degree with no burnt particles, greatly boosting product grade for domestic sales and overseas export.
Accurate Intelligent Control for Diverse Grain Varieties Equipped with PLC programmable controller and touch‑screen HMI, the unit allows operators to configure and store multiple custom curing profiles for different grains. Section‑wise stepless microwave‑power adjustment and frequency‑driven conveyor speed deliver fine‑tuned temperature, holding time and throughput for oats, quinoa, beans and grain powders. High‑precision temperature sensors keep temperature fluctuation within ±3℃. High process reproducibility guarantees uniform quality across production batches.
Combined Curing & Sterilization Meeting Export‑Grade Food Sanitation Standards While completing grain curing, drying and aroma optimization, microwave thermal and biological effects suppress microorganisms simultaneously. It deactivates E. coli, mold, insect‑eggs and other microbes by destroying their molecular structures and lowers initial microbial counts of raw materials. Fully enclosed automatic assembly‑line processing avoids secondary contamination from manual handling. Final products meet FDA and GMP sanitation requirements, ideal for cross‑border grains, meal‑replacement ingredients and functional cereal processing.
High‑throughput Continuous Production with Compact Footprint The fully‑automatic tunnel‑conveyor layout supports non‑stop 24‑hour operation. Feeding, curing, dehydration and discharging run automatically without manual attendance. Modular integrated design minimizes floor occupation while raising output. Custom‑tailored production lines with variable power, belt width and length are available, satisfying mass‑production demands for both small‑medium workshops and large‑scale grain deep‑processing manufacturers.
Safe, Hygienic & Eco‑friendly for Global Production Compliance Multi‑stage microwave‑suppression assemblies are installed at inlet and outlet, restricting microwave leakage ≤5 mW/cm² well below national safety limits for stable secure operation. All product‑contact components are built from food‑grade 304 stainless steel, featuring corrosion resistance, easy wash‑down and zero residual or dust contamination. Low‑temperature dry‑processing generates no waste gas, waste water or dust emissions. The eco‑friendly equipment complies with domestic and international food‑processing safety regulations.
Equipment Composition
Component | Function Description |
|---|---|
Microwave Generating System | The core energy‑producing unit fitted with premium‑grade industrial magnetrons. It delivers steady high‑frequency microwave output with even heat distribution, low energy consumption and long service life, supplying consistent energy for grain curing, aroma boosting and microbial suppression. |
Microwave Curing Cavity | Purpose‑built processing chamber optimized via professional electromagnetic simulation. Uniform microwave coverage eliminates dead zones, ensuring consistent curing degree and color across different grains. It prevents partial undercooking or scorching and stabilizes finished‑product quality batch‑to‑batch. |
Material Conveying System | Food‑grade non‑slip PTFE mesh belt featured with high temperature resistance, anti‑sticking property and easy‑to‑clean performance, complying with FDA food‑export specifications. Matched with variable‑frequency drive motors, conveyor speed can be fine‑tuned for different grain varieties and throughput targets to accommodate diverse curing workflows. |
Microwave Suppression System | Custom‑designed multi‑layer shielding assemblies are installed at inlet and outlet ends to effectively block microwave leakage. The equipment runs safely and fully complies with international manufacturing safety regulations. |
Moisture & Heat Exhaust System | Intelligent constant‑temperature moisture‑venting and heat‑dissipation units continuously remove water vapor and residual heat generated during grain curing. It precisely regulates material moisture content, prevents moisture re‑absorption and secures reliable curing‑drying outcomes. |
Automatic Control System | PLC touch‑screen based full‑auto control delivers user‑friendly operation. Multiple dedicated grain‑processing parameter sets can be preset and stored. One‑click start‑stop function supports accurate regulation of temperature, processing duration and conveyor speed. Unattended full‑process automation cuts labor costs and enables standardized mass production. |
Application Fields
Custom‑engineered for deep grain processing, the microwave grain curing equipment integrates curing, drying, aroma enhancement, sterilization and mildew‑proof functions. It is widely used for automated treatment of cereals, coarse grains and beans. Finished outputs feature crisp texture, rich aroma and extended shelf‑life. It serves food processing plants, dietary‑ingredient manufacturers, meal‑replacement powder factories and grain export enterprises. Key application categories are shown below:
Cereal Curing: Curing, drying, puffing and aroma improvement for oats, brown rice, black rice, millet, corn, sorghum, barley, quinoa and more. Suitable for producing instant cereals and breakfast grain raw materials.
Nut & Legume Processing: Low‑temperature curing, dehydration and sterilization for beans including red beans, mung beans, black beans, kidney beans, chickpeas, peanuts, sesame, as well as pistachios, almonds and other oil‑bearing nuts. It supplies standardized raw materials for grain powder, meal‑replacement formulas and healthy grain‑based snacks.
Grain‑Powder Pre‑treatment: Pre‑curing, sterilization and anti‑mildew handling for super‑fine cooked‑grain powder, multigrain meal‑replacement powder, nutritional formula powder and baking grain ingredients. Processed powder stays free of caking and meets microbial safety requirements.
Functional Whole‑grain Deep Processing: Curing and disinfection for medicinal‑edible grains and health‑oriented coarse grains, as well as export‑grade clean grain materials. Finished goods satisfy GMP and FDA international food standards for overseas raw‑material exports and cross‑border food supply chains.


