
Product Description
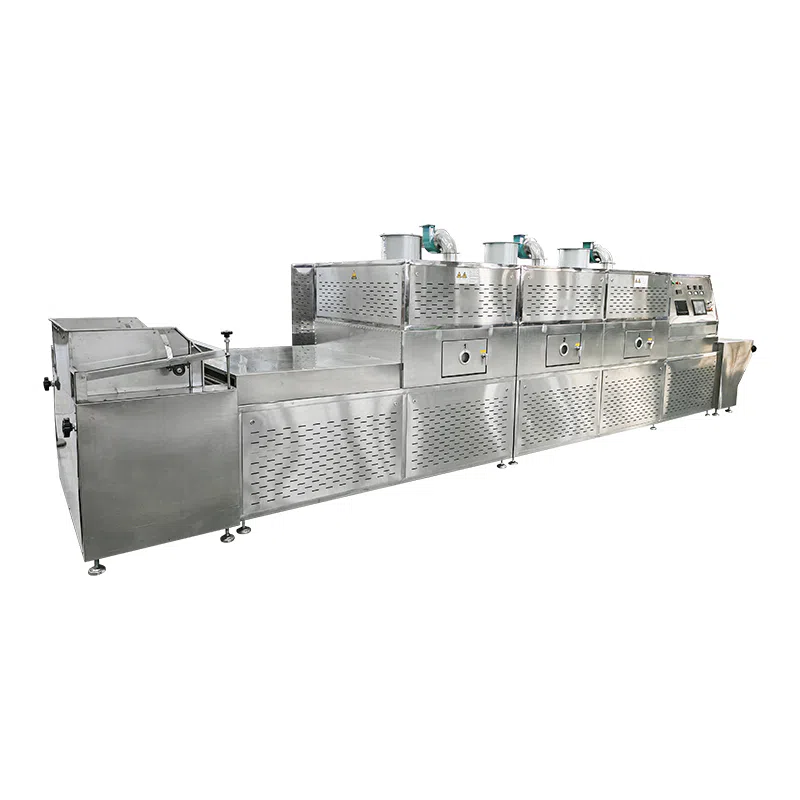
The insect microwave dehydration equipment applies high frequency 2450 MHz microwave energy directly to polar water molecules inside insect raw materials, including yellow mealworms, black soldier fly larvae, crickets and other protein rich insect materials. These molecules vibrate, rub and collide at an ultra high frequency of 2.45 billion times per second, rapidly converting electromagnetic energy into thermal energy to achieve uniform inside out dehydration of insect bodies.
Different from conventional hot air drying and oven drying, microwaves deliver excellent penetrative heating, achieving even temperature rise and consistent moisture removal throughout the insect material layer. It effectively solves typical industry drawbacks of traditional processing: uneven heating, surface over drying while the insect core remains damp, local scorching, protein denaturation, oil oxidation and inconsistent moisture content of finished insect protein products.
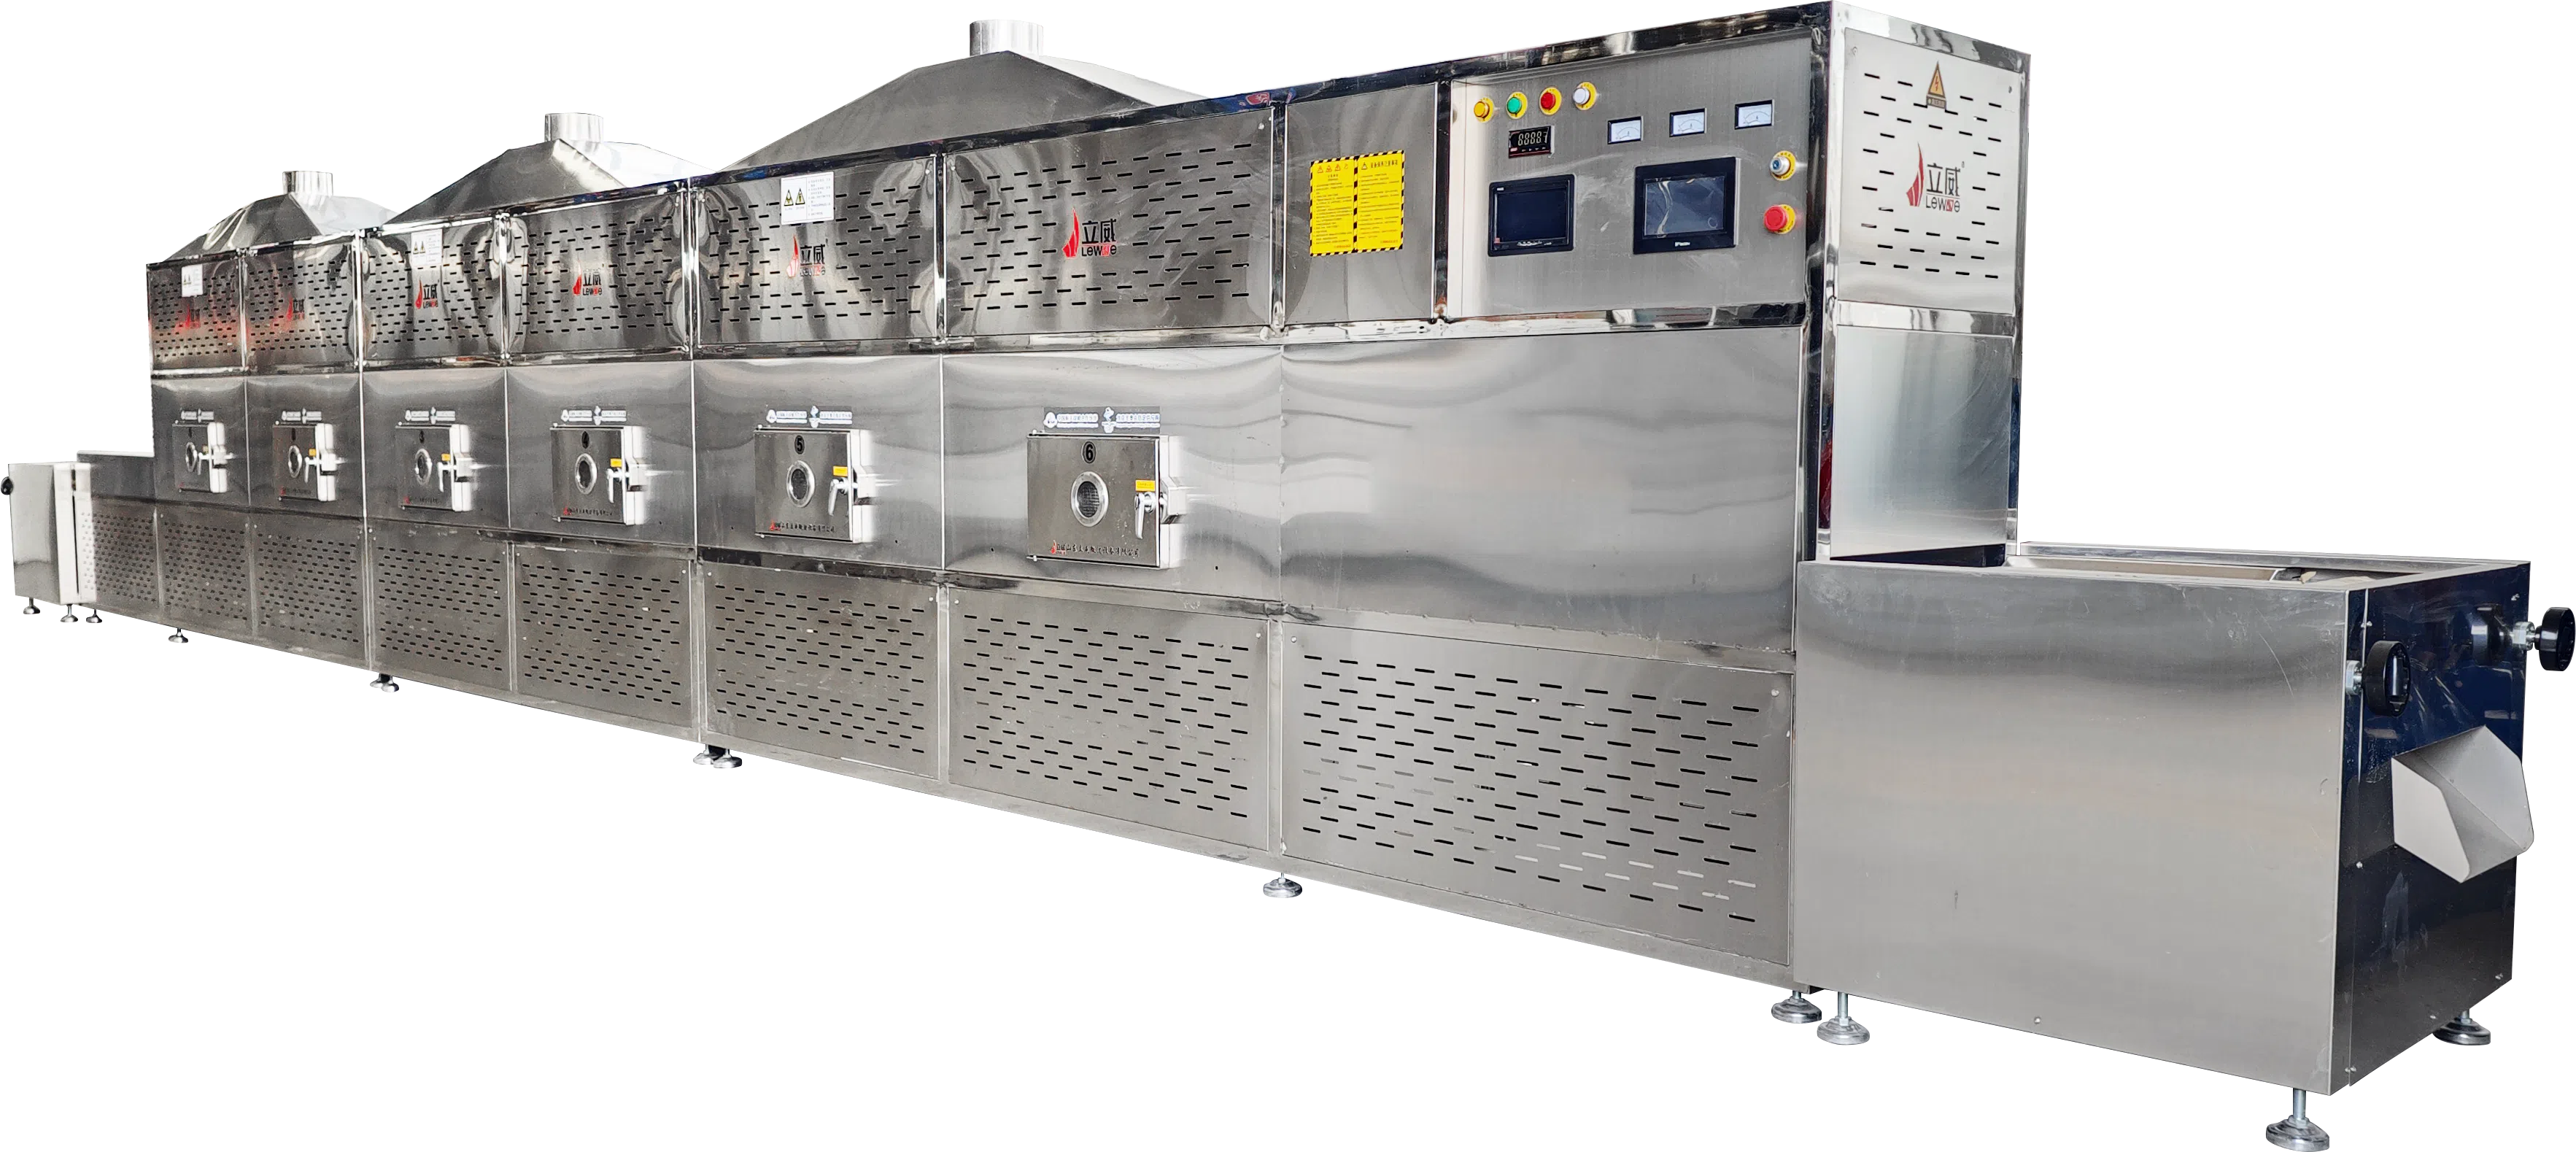
During operation, cleaned and pre screened wet insect larvae are evenly distributed on the wear resistant food grade conveyor belt and fed into the multi cascaded chamber microwave drying tunnel via variable frequency speed regulation. Microwaves penetrate the material layer for volumetric heating, quickly vaporizing internal free and bound water while performing synchronous sterilization and enzyme inactivation. A dedicated exhaust dehumidification system promptly evacuates water vapor and oil vapor, completing continuous integrated dehydration, drying, sterilization and shaping of insect protein products in one process.
The homogeneous microwave thermal field stabilizes physicochemical properties of insect materials and avoids excessive protein degradation and fat rancidity caused by local overheating. It removes residual moisture and volatile impurities, inhibits moisture re absorption, mildew and bacterial reproduction, greatly improves product color, protein retention rate and shelf life of dried insect products.
Main Advantages
Internal and External Synchronous Heating, Consistent Dehydration Quality
This insect microwave dehydration equipment adopts volumetric molecular heating rather than conventional surface heating. It realizes simultaneous heating from inside to outside of insect larvae, effectively eliminating core dampness, local over heating, scorching and uneven moisture caused by uneven thermal distribution. Finished dried insects feature uniform moisture, complete body shape and stable protein content, raising the overall product qualification rate.
Mild Low Temperature Dehydration, Maximize Protein Retention
The equipment performs mild low temperature constant temperature dehydration, protecting protein, amino acids and fat components inside insects. While removing excess moisture, it reduces fat oxidation and protein denaturation induced by high temperature processing. It is especially suitable for high protein insect raw materials used for animal feed, pet food and food additive industries.
Intelligent Adjustable Process, Strong Adaptability for Multiple Insect Varieties
Equipped with a PLC intelligent control system, the unit supports stepless adjustment of microwave power, conveyor speed, temperature and exhaust volume. It fits diverse dehydration requirements for yellow mealworms, black soldier fly larvae, crickets and other insect raw materials. Modular integrated structure ensures stable long time running with convenient daily maintenance and parameter debugging.
Efficient Continuous Production, Thorough Sterilization and Extended Shelf Life
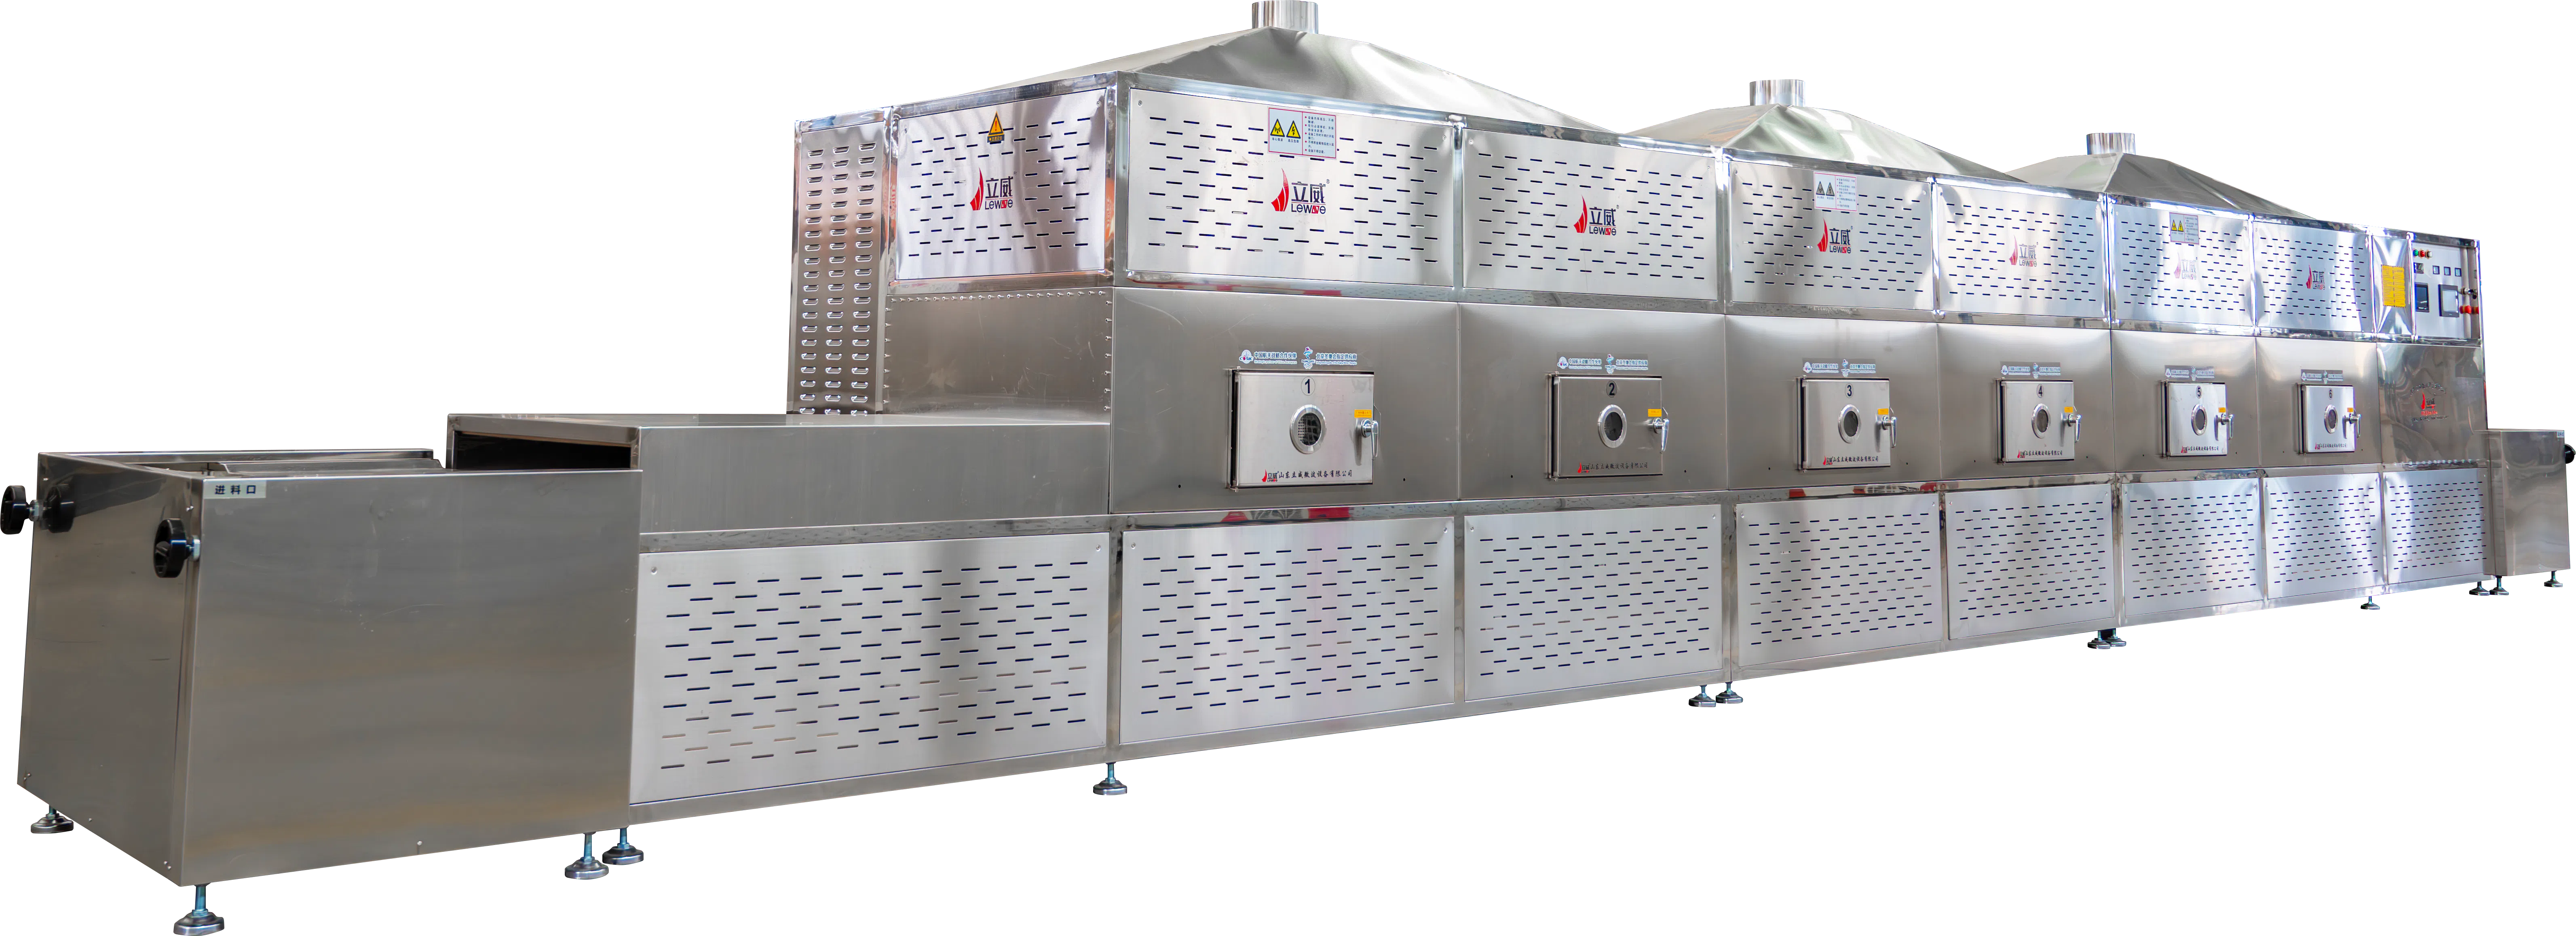
Fitted with multi stage microwave shielding and closed food grade drying chamber, the equipment reaches ultra low microwave leakage complying with international safety standards. Microwave treatment realizes synchronous sterilization to suppress harmful microorganism reproduction. The fully automatic tunnel production line enables non stop unmanned operation, greatly shortening dehydration cycles compared with traditional hot air drying. Treated insect materials resist moisture re absorption, fat oxidation and mildew, extending storage time for feed factories, pet food brands and export grade insect protein applications.
Equipment Composition
The insect microwave dehydration equipment adopts a fully automatic tunnel type assembly line structure with food grade anti pollution modular design. It runs steadily, meets feed and food hygiene requirements and allows easy maintenance. The complete set consists of multiple core functional systems including feeding, material spreading, microwave dehydration, exhaust dehumidification, oil fume collection, intelligent temperature control and automatic discharging. It is well suited for large scale standardized dehydration and drying of various insect protein raw materials.
Application Fields
The insect microwave dehydration equipment is custom developed for insect protein processing, feed manufacturing and pet snack industries. It is widely used for low temperature dehydration, drying, sterilization and mildew proof treatment of various insect raw materials. Processed insect materials show stable color, uniform moisture and high retained protein value. It serves insect processing plants, feed manufacturers and insect protein export enterprises.


