
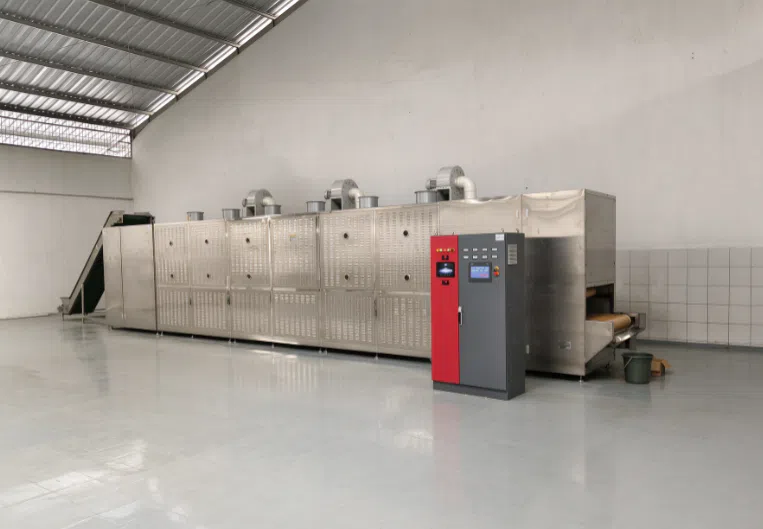
Client Profile: Local professional spice processing and manufacturing enterprise
Service Provider: Shandong Lewave Group Company
Project Completion: On-site installation, commissioning and official production launch
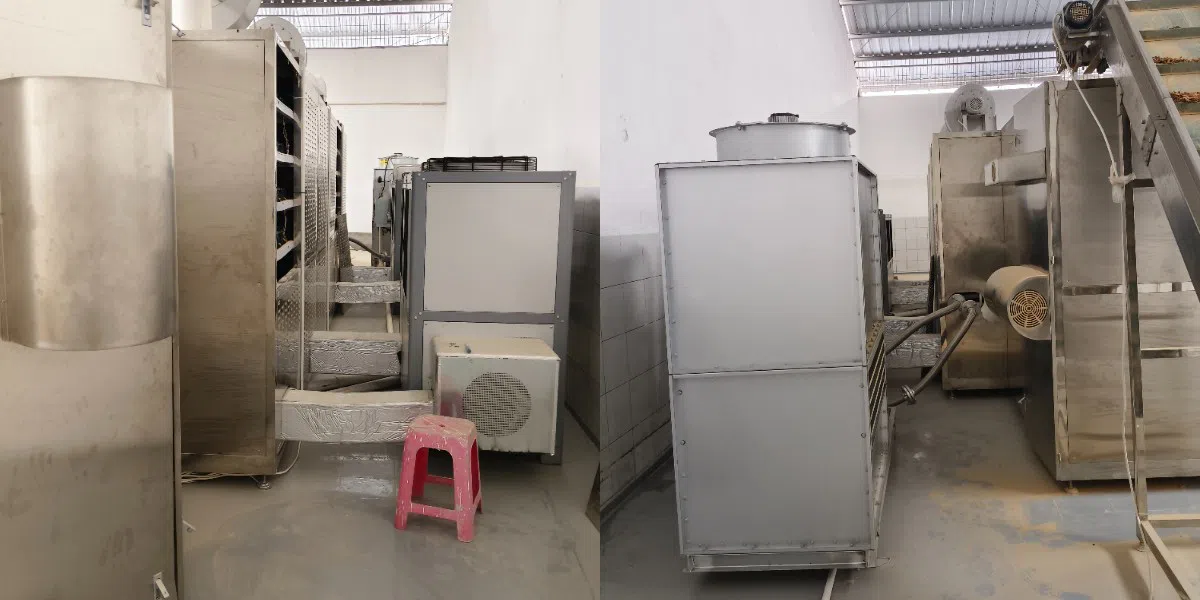
Project Background & Client Pain Points
The Ethiopian local spice industry has long relied on traditional high-temperature drying and chemical disinfection methods. For this client, the outdated processing technology brought multiple production and quality bottlenecks that restricted business expansion.
Traditional sterilization caused serious loss of spice natural flavor and color, while chemical disinfection led to residual problems, making it impossible for their products to meet international food export standards. In addition, the original intermittent production equipment could not support large-volume order output, with unstable sterilization effect and high microbial excess rate, which greatly limited the client’s market competitiveness and product sales radius.
Customized Solution by Lewave
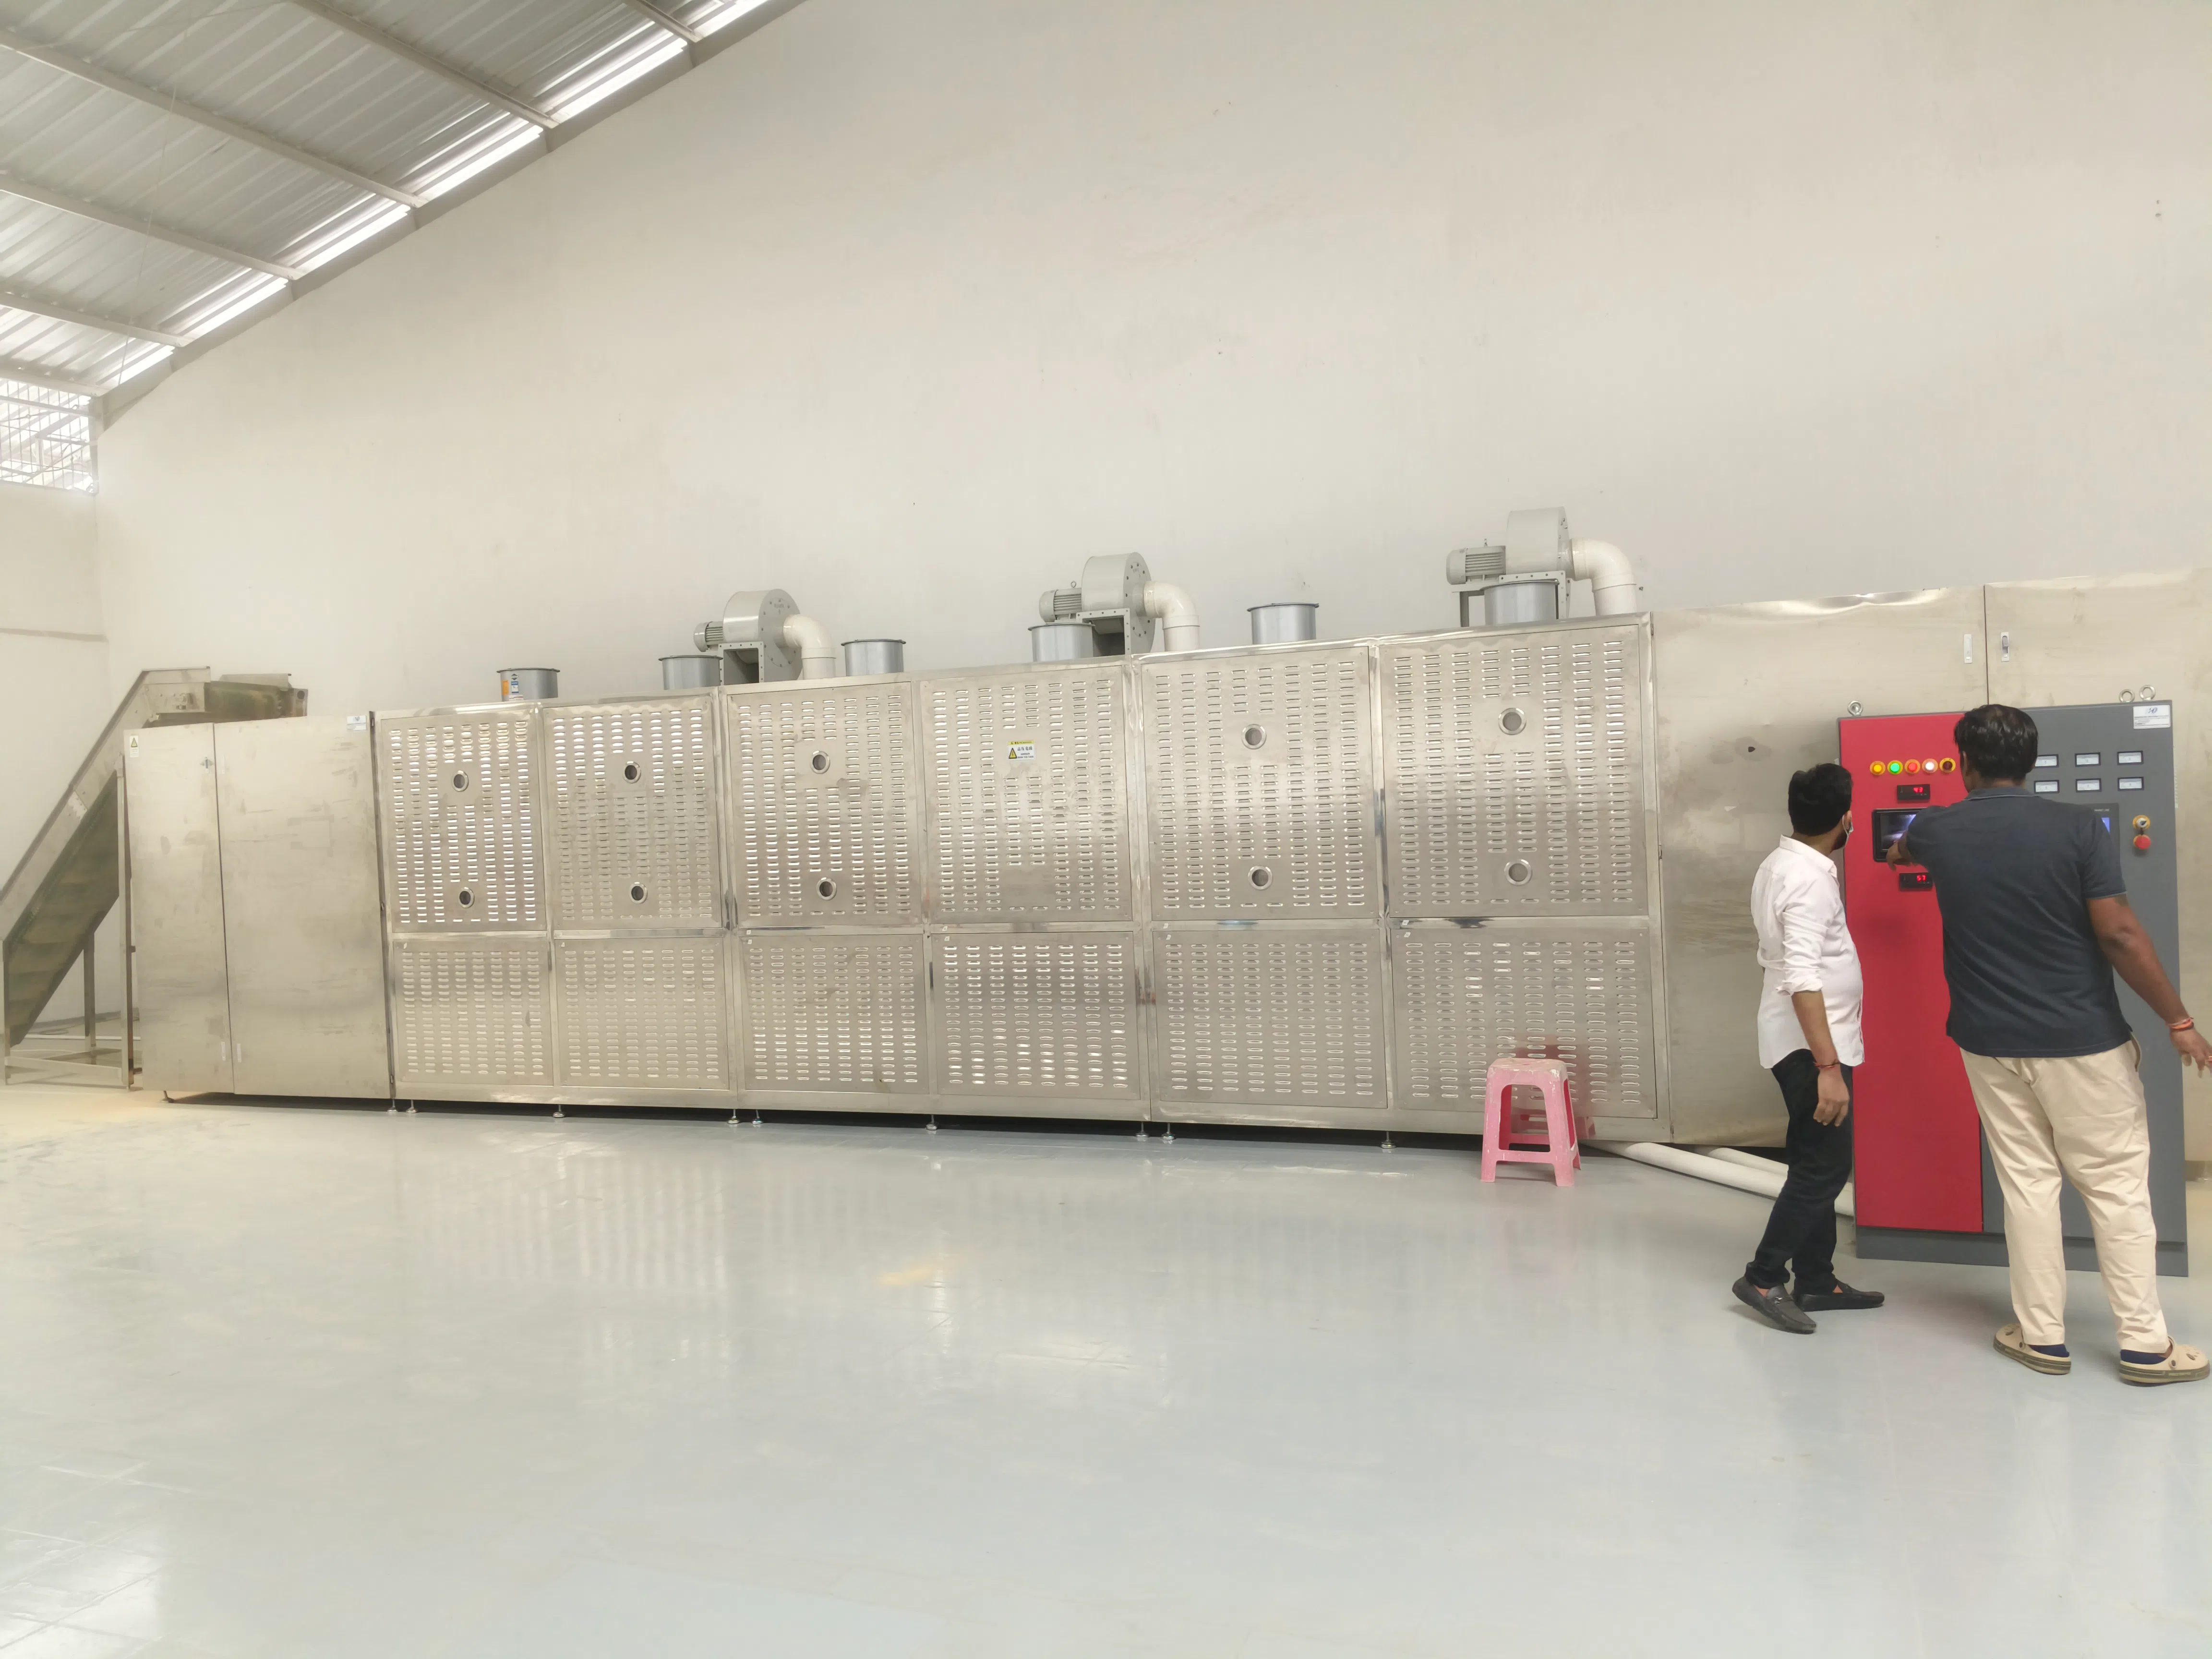
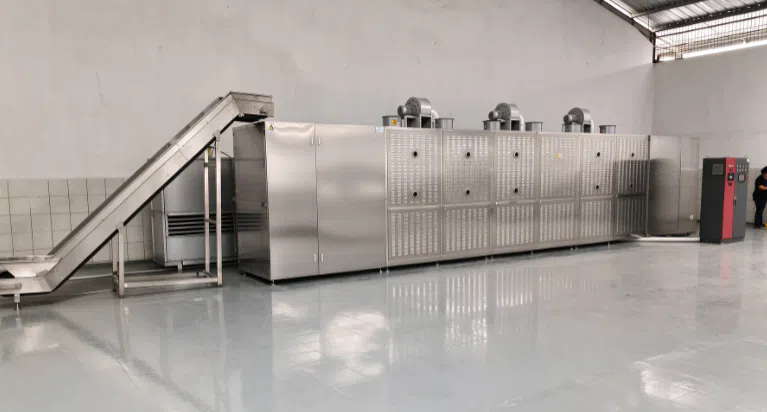
After in-depth communication and analysis of the client’s local production conditions, spice types and export quality requirements, Shandong Lewave Group Company customized a set of 120kW tunnel-type continuous microwave physical sterilization solutions for the client.
Different from conventional processing methods, our solution adopts low-temperature microwave physical sterilization technology, which solves the client’s core pain points of flavor damage, chemical residue and unqualified sterilization rate. The fully continuous tunnel production mode perfectly matches the client’s large-scale and standardized production needs. Meanwhile, the equipment is optimized and upgraded targeting Ethiopia’s local climate and factory environment, ensuring stable long-term operation.
On-site Implementation & Full-cycle Service
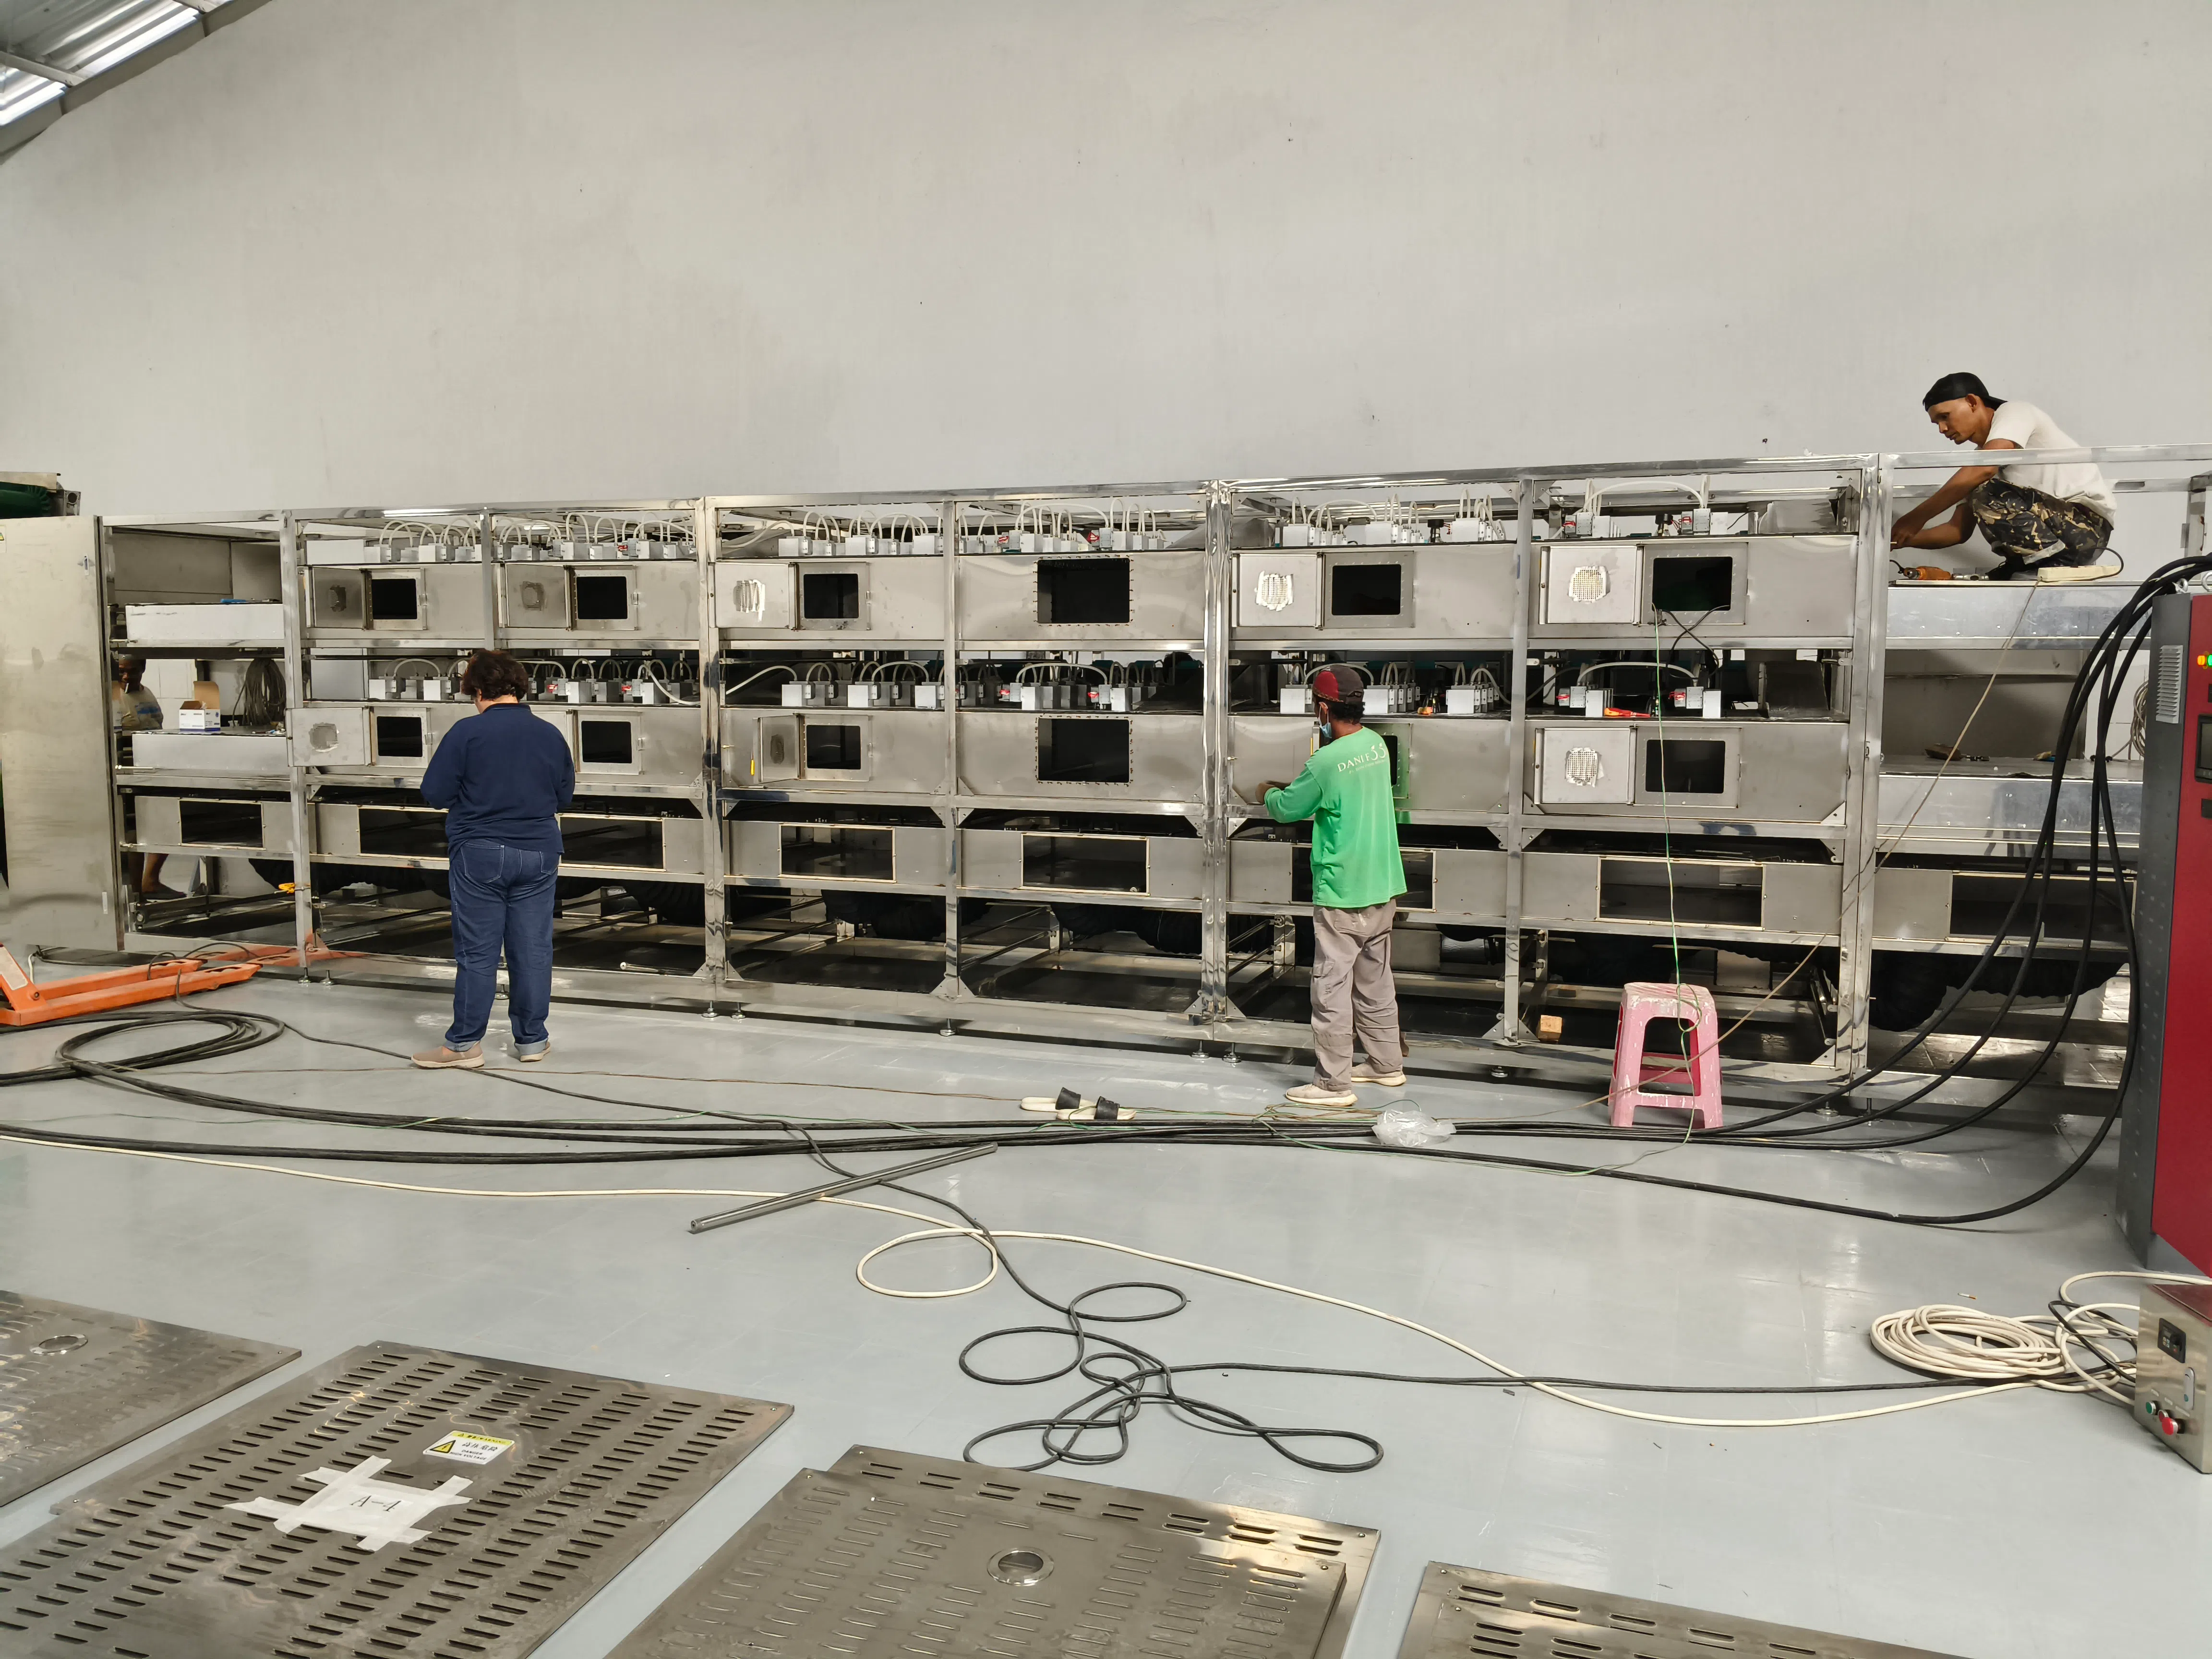
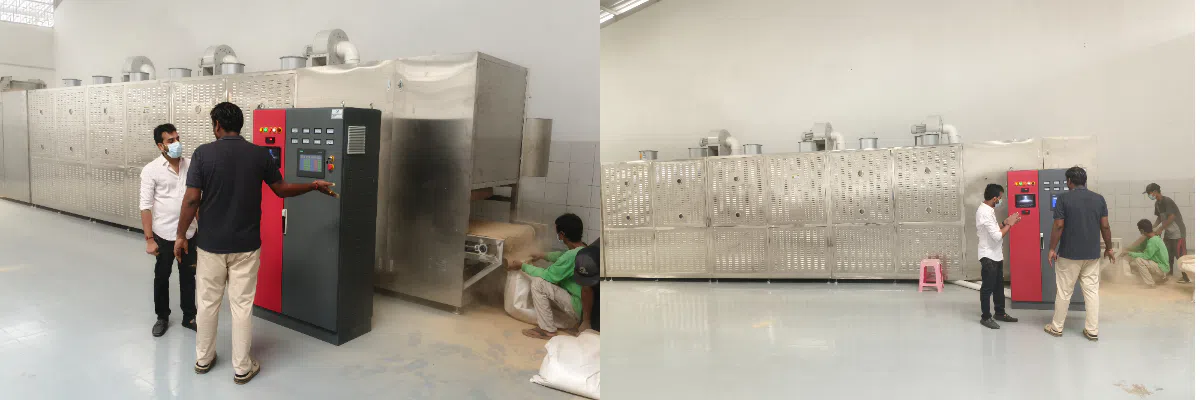
To ensure smooth project landing, Lewave provided one-stop overseas turnkey services for this Ethiopia project. Our professional overseas technical team went to the client’s factory site to conduct full-process installation guidance, equipment commissioning, production debugging and operator technical training.
During the implementation period, our team guided the client’s staff to master equipment operation, daily maintenance and fault handling skills, helping the production line quickly complete trial production and formal mass production. We also established long-term remote after-sales technical support to guarantee stable and efficient operation of the production line all year round.
Project Operation Results & Client Benefits
After the official operation of the Lewave microwave sterilization production line, the client’s spice processing quality and production capacity have been comprehensively upgraded, achieving remarkable improvement:
Qualified Rate Upgrade: The sterilization rate reaches 99.9%, effectively killing E. coli, salmonella, mold and other harmful bacteria. The microbial indicators fully meet local and international food safety standards.
Product Quality Optimization: Low-temperature sterilization at 75–85℃ completely retains the natural aroma, color and nutritional ingredients of spices, with zero chemical residues. The product grade is greatly improved, supporting export business expansion.
Production Efficiency Improvement: Continuous automatic production replaces traditional intermittent processing, realizing 24-hour stable production, greatly increasing daily output and effectively shortening order delivery cycle.
Production Cost Reduction: The equipment features stable operation, low energy consumption and simple maintenance, effectively reducing the client’s long-term production and labor costs.
Project Summary
This Ethiopia spice sterilization project is a successful practice of Lewave’s customized industrial microwave solutions for African food processing enterprises. Relying on mature technology, targeted customized design and professional overseas on-site services, Shandong Lewave Group Company has helped local clients solve long-standing production quality problems, realize standardized and large-scale production, and lay a solid foundation for their brand upgrading and market expansion. It also further proves Lewave’s professional strength and service capability in overseas industrial microwave equipment turnkey projects.


